-
- Products
- Indoor Household Cords
- Appliance Cords
- General Purpose Short-Length Cords
- General Purpose Extension Cords
- Landscape & Decorating Cords
- Bright Color Extension Cords
- Oil-Resistant Extension Cords
- Cold-Flex Extension Cords
- VividFlex Power Cords
- EXTREME All-Weather Cords
- Cord Management
- Task Lights
- Adapters & GFCI Devices
- Where to Buy
- About
- Careers
- Glossary
- Catalog

2026 Best Powder Pressing Machine Buying Guide?
Choosing the right Powder Pressing Machine in 2026 requires more than comparing pressure ratings or attractive price tags. Powder behavior, tooling design, production volume, and final part density must work together. A machine that performs well with ceramic powder may struggle with metal powders or fragile pharmaceutical-grade materials. The details matter.
Dr. Randall M. German, a respected powder metallurgy researcher, has emphasized, “Powder processing controls the final structure and properties.” This principle should guide every buying decision. A reliable buyer will inspect compaction force, filling accuracy, die alignment, press speed, control systems, and energy consumption. Ask for test results using your actual powder. Do not trust a polished brochure alone. Request density maps, cycle-time data, maintenance records, and references from comparable factories.
Look closely at the working area. Can operators clean the feed system without wasting material? Does the frame remain stable during repeated pressing? Small vibrations can create uneven density, visible cracks, or inconsistent dimensions. These defects may appear only after sintering, when correction becomes expensive.
Safety and service support also deserve attention. Guarding, emergency stops, dust control, training, spare parts, and remote diagnostics can influence long-term reliability. A cheaper Powder Pressing Machine may become costly when downtime and tooling changes accumulate. However, the most expensive model is not automatically the best choice. Your material, part geometry, and output target should decide.
This guide examines practical specifications, common mistakes, supplier questions, and ownership costs. Some recommendations remain conditional. Real production trials still matter. That is where confident assumptions often fail.
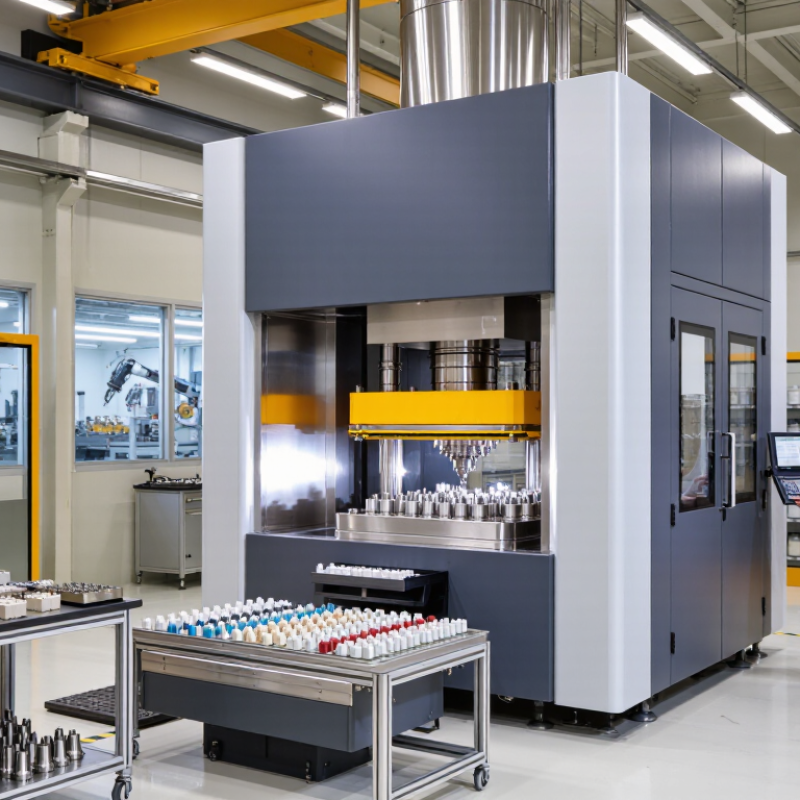
Table of Contents [Hide]
What Is a Powder Pressing Machine?
A powder pressing machine compacts loose powder inside a shaped die. Pressure creates a “green compact,” which keeps its form before sintering or another finishing process. The machine does not melt the material. It controls force, movement, filling, and ejection.
Common systems use hydraulic, mechanical, or servo-driven presses. A typical cycle includes die filling, pre-compression, main pressing, and controlled release. Operators check powder flow, moisture, particle size, and lubrication because small changes can produce cracks or uneven density. The International Organization for Standardization describes apparent density testing in ISO 3923-1, showing why powder behavior matters before pressing. A dense-looking part can still be weak inside.
Industry demand is growing. Grand View Research valued the global powder metallurgy market at about USD 2.7 billion in 2023 and projected a 6% annual growth rate through 2030. Fortune Business Insights also identifies automotive, industrial, and electrical applications as major demand areas. These figures describe the wider market, not machine sales alone. That distinction is easy to miss.
Choosing equipment requires more than comparing maximum tonnage. Review die dimensions, target density, cycle speed, powder characteristics, and ejection control. In practical testing, a press may meet its rated force yet deliver inconsistent parts. That is a warning sign. Measure density at several locations, inspect edges under magnification, and record every setup change. Production data should guide the purchase, although early test results can still mislead when the powder blend changes.