-
- Products
- Indoor Household Cords
- Appliance Cords
- General Purpose Short-Length Cords
- General Purpose Extension Cords
- Landscape & Decorating Cords
- Bright Color Extension Cords
- Oil-Resistant Extension Cords
- Cold-Flex Extension Cords
- VividFlex Power Cords
- EXTREME All-Weather Cords
- Cord Management
- Task Lights
- Adapters & GFCI Devices
- Where to Buy
- About
- Careers
- Glossary
- Catalog

2026 Top Carbon Fiber Production Line Manufacturers?
The 2026 carbon fiber market will reward stable production, not impressive brochures. A modern Carbon fiber production line factory must control precursor quality, oxidation, carbonization, surface treatment, and winding accuracy. Each stage affects tensile strength, modulus, yield, and energy consumption. Small temperature changes can alter the final tow. That detail matters.
Dr. Akio Shindo, a pioneer of PAN-based carbon fiber development, emphasized a lasting production principle: “Stable processing is essential for consistent carbon fiber quality.” His work reminds buyers that equipment design cannot replace process discipline. Leading manufacturers should demonstrate furnace uniformity, tension control, atmosphere management, and reliable line integration. They should also provide traceable testing data. Claims without production evidence deserve caution.
This review examines the top carbon fiber production line manufacturers expected to influence 2026. It considers engineering experience, automation depth, maintenance support, energy performance, and customization capability. Practical evidence matters more than polished marketing. A strong supplier should explain commissioning procedures and failure-response plans. It should also show how the line performs during long, continuous runs.
Not every high-speed line delivers better economics. That assumption can fail. Excessive speed may increase breaks, scrap, or unstable surface treatment. Buyers should compare usable output, not only rated capacity. They should inspect factory references, sample fiber data, spare-parts access, and operator training. Regional service coverage may become decisive. This guide therefore balances technical performance with commercial reliability, while acknowledging one uncomfortable truth: even advanced lines require skilled people, careful calibration, and ongoing improvement.
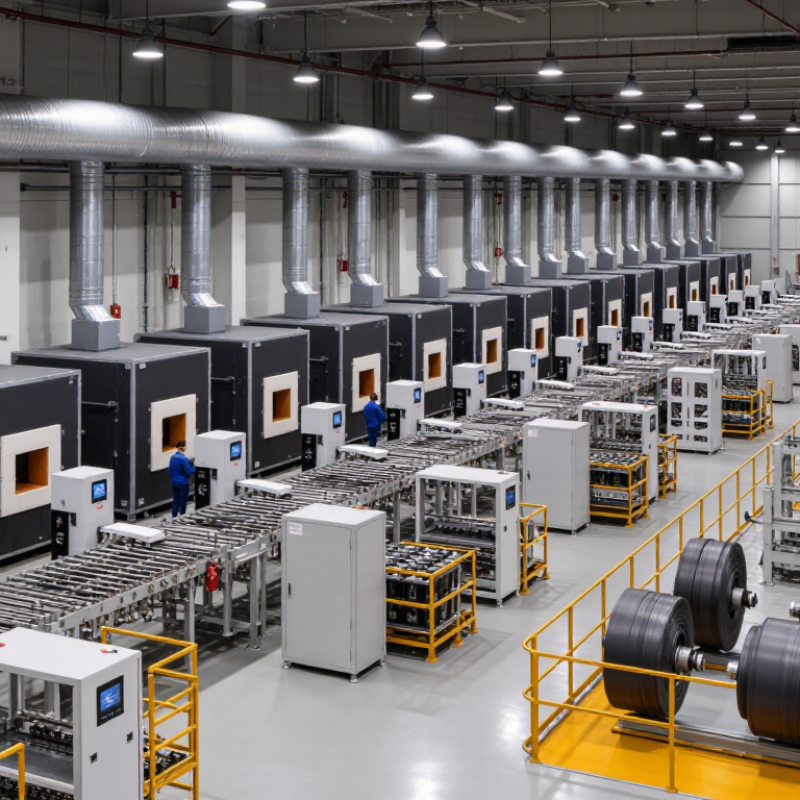
Table of Contents [Hide]
What Is a Carbon Fiber Production Line?
A carbon fiber production line is an integrated industrial system that converts polymer precursor into strong, lightweight carbon fiber. In practical plant work, the line feels less like one machine and more like a carefully timed chain. It typically includes precursor unwinding, stabilization ovens, carbonization furnaces, surface treatment, sizing, drying, and final winding. Each section changes the filament gradually. The fiber may look unchanged to the eye. Inside, its molecular structure is becoming more heat-resistant and ordered.
During stabilization, controlled heat and airflow prevent the precursor from melting. Carbonization then removes non-carbon elements in oxygen-limited furnaces. Temperatures can exceed 1,000°C, so furnace sealing and gas monitoring matter greatly. Line speed, tension, residence time, and temperature must remain coordinated. A small tension drift can create fuzz, breaks, or uneven tow packages. Operators inspect fiber surfaces, check tensile samples, and compare furnace data with production records. That part matters. These details reveal whether the process is stable, not merely whether the line is running.
A reliable line also needs alarms, interlocks, exhaust treatment, calibration routines, and traceable quality records. Surface treatment improves bonding with resins, while sizing protects filaments during handling. The design depends on tow size, target strength, energy use, and required output. No line is perfect. In my view, early trials often expose overlooked heat loss or difficult maintenance access. Those findings should change the layout before full-scale production begins. A polished specification can still hide practical weaknesses.