-
- Products
- Indoor Household Cords
- Appliance Cords
- General Purpose Short-Length Cords
- General Purpose Extension Cords
- Landscape & Decorating Cords
- Bright Color Extension Cords
- Oil-Resistant Extension Cords
- Cold-Flex Extension Cords
- VividFlex Power Cords
- EXTREME All-Weather Cords
- Cord Management
- Task Lights
- Adapters & GFCI Devices
- Where to Buy
- About
- Careers
- Glossary
- Catalog

What Are the 2026 Top Painting Line Types for Buyers?
Choosing a Painting Line in 2026 requires more than comparing speed, price, and supplier brochures. Buyers must study the complete production picture. That includes coating type, substrate, curing method, floor space, energy demand, maintenance access, and operator training. A line that looks efficient on paper may create bottlenecks beside the oven or spray booth. Small details matter. Overspray becomes visible quickly.
Industrial finishing consultant Michael R. Miller states, “The best painting line is the one that delivers stable quality, not simply higher speed.” This principle deserves attention when evaluating powder coating lines, liquid spray systems, electrophoretic lines, and UV-curing equipment. Each type serves different products and production targets. Powder systems often suit durable metal parts. Liquid systems offer broader color and finish flexibility. Electrophoretic coating supports consistent coverage on complex components. UV technology can reduce curing time, but only when materials and equipment align correctly.
The strongest 2026 options will combine automation with practical human control. Robotic guns, sensors, data monitoring, and automatic color changes can improve repeatability. Yet advanced features may increase training demands and repair costs. That is easy to overlook. Buyers should request sample panels, energy figures, coating-transfer results, and references from comparable factories. They should also examine cleaning time between colors. A beautiful specification is not enough. Real performance appears during the third shift, when filters load, temperatures fluctuate, and skilled technicians must respond. This guide compares the leading Painting Line types through that practical lens, while recognizing that no single system fits every buyer.
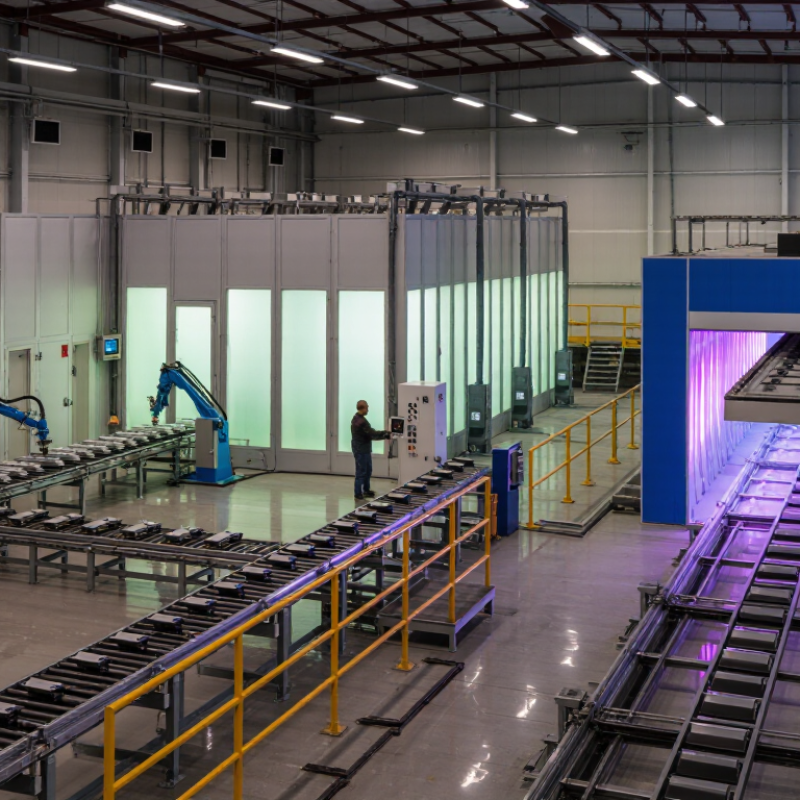
Table of Contents [Hide]
What Painting Line Types Are Available to Buyers in 2026?
In 2026, buyers can choose from several painting line types, depending on product size, material, and production volume. Manual spray lines suit small workshops and frequent color changes. They need limited equipment, but finish consistency depends heavily on operator skill. A compact spray booth, filtered airflow, and a controlled drying area are essential details.
Batch powder coating lines work well for metal parts produced in mixed sizes. Operators load parts onto racks, apply powder, and cure them inside an oven. This setup reduces overspray waste and supports durable finishes. Buyers should check oven temperature uniformity, ventilation capacity, and rack loading limits. These details often affect real output more than advertised line speed.
Automated conveyor painting lines suit large, repeatable production. They may include pretreatment, spraying, curing, cooling, and inspection sections. Sensors can monitor temperature, coating thickness, and conveyor movement. Dip coating and electrocoating lines are also available for parts requiring even coverage around edges or internal surfaces. They usually demand higher installation costs and stricter process control. Not every factory needs that complexity.
In factory assessments, I have seen buyers underestimate floor space and maintenance access. That mistake becomes expensive. Energy recovery systems can lower operating costs, but their value depends on daily production hours. A reliable supplier should provide airflow data, curing tests, safety documentation, and training records. Buyers should request sample panels before approval. Even then, one test may not represent every future material or color.