-
- Products
- Indoor Household Cords
- Appliance Cords
- General Purpose Short-Length Cords
- General Purpose Extension Cords
- Landscape & Decorating Cords
- Bright Color Extension Cords
- Oil-Resistant Extension Cords
- Cold-Flex Extension Cords
- VividFlex Power Cords
- EXTREME All-Weather Cords
- Cord Management
- Task Lights
- Adapters & GFCI Devices
- Where to Buy
- About
- Careers
- Glossary
- Catalog

10 Best Gummy Making Machines for Your Business?
The global gummy category is expanding beyond traditional confectionery. Fortune Business Insights reports continued growth in gummy products through 2032, driven by supplements, functional ingredients, and convenient portion formats. Grand View Research also identifies gummies as a fast-growing segment within the broader nutraceutical market.
That growth creates pressure on manufacturers. A reliable Gummy Making Machine must deliver consistent weight, shape, texture, and color across thousands of pieces. It should also support accurate depositing, controlled cooking temperatures, hygienic material handling, and efficient cooling. Small errors become expensive quickly. A one-gram filling variation can affect product cost, labeling accuracy, and customer trust.
PMMI industry reports repeatedly highlight automation, labor efficiency, and flexible production as major packaging concerns. These priorities also influence gummy production equipment. A small startup may need compact changeovers, while a large factory may prioritize continuous output and automated cleaning. Neither option is universally best. It depends on recipe viscosity, mold design, batch size, staffing, and facility layout.
This guide compares ten leading machines for business use. Each option is considered through practical criteria, including output capacity, temperature control, sanitation access, maintenance demands, and technical support. Food safety remains essential. Buyers should verify applicable GMP, HACCP, FDA, or regional requirements before purchase.
No machine is perfect.
A polished specification sheet can still hide difficult cleaning procedures or costly replacement parts. That is why real operating details matter. The best Gummy Making Machine is not always the fastest model. It is the machine that fits your product, budget, workforce, and long-term production goals.
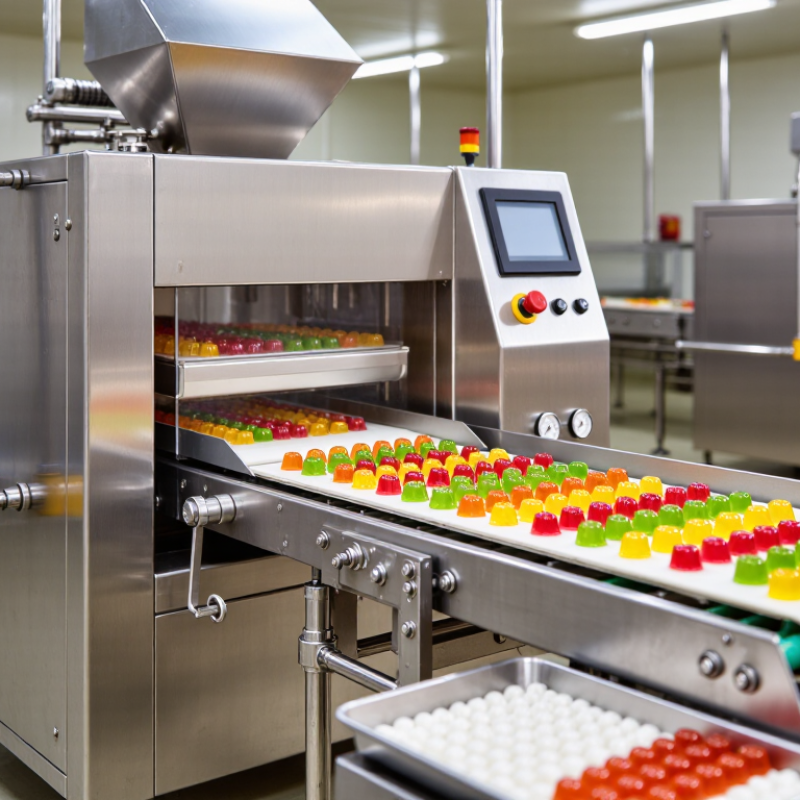
Table of Contents [Hide]
What to Consider When Choosing a Gummy Making Machine
What to Consider When Choosing a Gummy Making Machine
Gummy demand is growing, but growth alone should not decide your equipment purchase. Grand View Research valued the global gummy market at about $19.1 billion in 2023 and projected a 12.6% annual growth rate through 2030. That pressure can make high-speed machinery attractive. However, a machine must match your actual batch size, recipe viscosity, and production schedule. A compact depositor may outperform a larger system when orders remain unpredictable.
Check the dosing range, heating control, mold changeover, and cooling capacity. A reliable machine should maintain consistent piece weight across long runs. Ask for measured output, not only advertised speed. PMMI’s 2024 industry research highlights automation, flexible equipment, and labor efficiency as major packaging priorities. Those priorities also matter in gummy production. Still, automation cannot fix poor formulation control. A warm room, uneven syrup temperature, or weak cleaning routine can create sticking and waste.
Hygiene deserves close attention. Look for food-contact surfaces, tool-free access, documented cleaning procedures, and clear allergen controls. Verify whether operators can inspect pumps and nozzles without dismantling half the line. That detail matters during a midnight sanitation check. Calculate total ownership cost, including molds, utilities, maintenance, training, and rejected batches. I would also request a live trial with your own formulation. Sales demonstrations often use easier recipes. That is where careful buyers should remain skeptical.