-
- Products
- Indoor Household Cords
- Appliance Cords
- General Purpose Short-Length Cords
- General Purpose Extension Cords
- Landscape & Decorating Cords
- Bright Color Extension Cords
- Oil-Resistant Extension Cords
- Cold-Flex Extension Cords
- VividFlex Power Cords
- EXTREME All-Weather Cords
- Cord Management
- Task Lights
- Adapters & GFCI Devices
- Where to Buy
- About
- Careers
- Glossary
- Catalog

What Is the Best MCB Inspection Conveyor in China?
Choosing the best Mcb Inspection Conveyor in China requires more than comparing prices and photographs. The right system must support stable feeding, precise positioning, reliable inspection, and controlled product discharge. It should also fit the manufacturer’s production rhythm. A fast conveyor is not automatically a good conveyor.
In practical factories, small details often decide performance. Adjustable guides should hold miniature circuit breakers without scratching their housings. Sensors must detect gaps, double feeding, and misalignment. Vision cameras need steady lighting and a clean inspection window. A responsive PLC can connect inspection results with automatic rejection and production records. Maintenance access matters too. Dust gathers. Belts stretch. Operators need quick solutions.
According to electrical automation specialist Dr. Martin Keller, “A conveyor proves its value when it protects inspection accuracy, not merely production speed.” That principle offers a useful starting point for this article. The best Mcb Inspection Conveyor should combine mechanical stability, inspection compatibility, safety design, and dependable after-sales support in China. Suppliers with documented testing, clear electrical drawings, and factory references deserve closer attention. Claims alone are not enough.
No machine is perfect. A promising design may still struggle with unusual breaker shapes, reflective surfaces, or inconsistent upstream feeding. That assumption needs testing. Buyers should request sample trials using their own products, speeds, and inspection requirements. They should also review changeover time, spare-part availability, software support, and operator training. This introduction examines these practical factors and explains how to compare Chinese conveyor manufacturers with greater confidence.
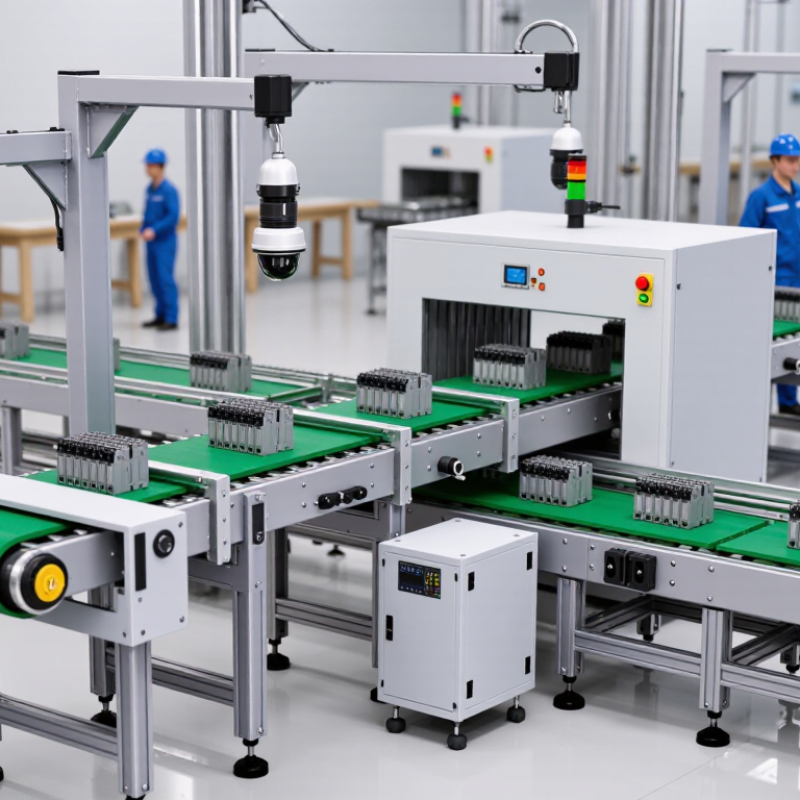
Table of Contents [Hide]
What Is an MCB Inspection Conveyor?
An MCB inspection conveyor is a production-line system that moves miniature circuit breakers through controlled inspection points. It does more than transport parts. It positions each MCB accurately for checking, testing, and safe removal.
A typical conveyor uses fixtures, indexing mechanisms, sensors, and vision cameras. These components inspect housing appearance, terminal position, label accuracy, and assembly completeness. Some systems also connect with electrical testing equipment. The conveyor pauses each unit briefly, allowing stable measurements and consistent results. A reject mechanism then separates defective products from approved ones. Clear records help engineers trace batch numbers, inspection results, and machine alarms.
The best MCB inspection conveyor in China should match the product design, output target, and factory layout. Stable positioning matters more than impressive speed. In practical production, dust, vibration, and fixture wear can affect accuracy. Regular cleaning and calibration are necessary. Small errors grow quickly. Operators should also access sensors and fixtures without complicated procedures. A reliable system includes emergency stops, guarded moving parts, and understandable control screens. However, no conveyor is perfect for every MCB model. New designs may require fixture changes or software adjustments. Trial production can reveal problems that specifications miss. That uncomfortable step is often valuable.