-
- Products
- Indoor Household Cords
- Appliance Cords
- General Purpose Short-Length Cords
- General Purpose Extension Cords
- Landscape & Decorating Cords
- Bright Color Extension Cords
- Oil-Resistant Extension Cords
- Cold-Flex Extension Cords
- VividFlex Power Cords
- EXTREME All-Weather Cords
- Cord Management
- Task Lights
- Adapters & GFCI Devices
- Where to Buy
- About
- Careers
- Glossary
- Catalog

10 Blister Retail Packaging Tips for Global Buyers
Blister Retail Packaging is more than a clear plastic shell around a product. It is a compact sales tool, protection system, and communication surface. Global buyers must examine each detail, from cavity size and card stiffness to opening effort and shelf visibility. A small design weakness can create crushed corners, trapped moisture, or confusing product information during international distribution.
Walter Soroka, a respected packaging educator, described packaging as “the science, art and technology of enclosing products for protection, distribution, storage, sale and use.” His definition remains practical for today’s retail blister projects. Good packaging should protect a product through handling, support efficient merchandising, and help customers understand what they are buying. It should also suit local recycling expectations, production capabilities, and consumer habits.
Details matter.
These ten tips focus on real purchasing decisions. They address material selection, sealing quality, artwork consistency, tamper visibility, shipping tests, and supplier communication. Buyers should request samples before approving large production runs. A package that looks excellent on a computer screen may feel awkward in a customer’s hands. It may also require more material than necessary.
There is no universal blister solution. A design that performs well in a dry warehouse may struggle in humid transport conditions. Some assumptions will be wrong. That is why measurable testing, supplier experience, and thoughtful revision remain essential. Reliable Blister Retail Packaging is not created by appearance alone. It is refined through evidence, practical feedback, and careful attention to the final retail environment.
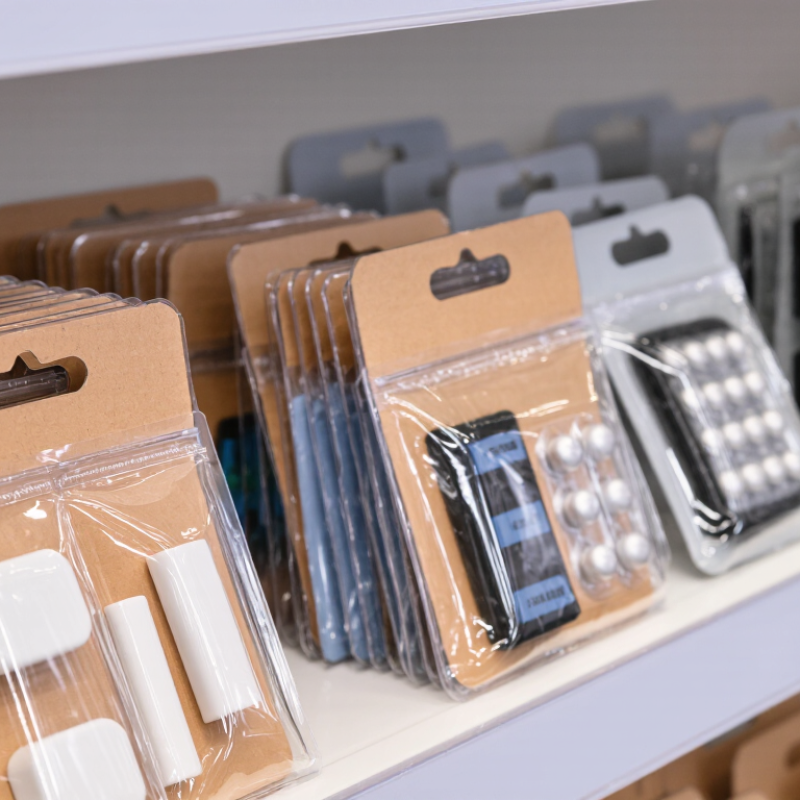
Table of Contents [Hide]
Define Product Requirements and Target Market Standards
Define Product Requirements and Target Market Standards
A reliable blister specification starts with the product, not the packaging machine. Record tablet dimensions, breakability, moisture sensitivity, light sensitivity, dosage instructions, and shelf-life targets. A 0.25-millimeter size change can affect cavity fit and sealing pressure. Small details matter.
Target-market standards must be mapped before sampling. For pharmaceutical products, ISO 15378 supports quality management for primary packaging materials. ISO 11607 addresses sterile barrier packaging where applicable. Distribution testing may follow ASTM D4169 or ISTA procedures. Requirements also differ by climate. A humid coastal market may need stronger moisture protection than a dry inland region. Add local language, required warnings, recycling marks, and accessibility expectations to the artwork brief. Check every translation.
The World Health Organization estimates that one in ten medical products in low- and middle-income countries is substandard or falsified. Packaging cannot solve every supply-chain risk, but clear identifiers, tamper evidence, and consistent seal inspection can reduce avoidable failures.
Use measurable limits for seal strength, leak rates, cavity depth, and print contrast. Smithers’ global packaging research also places sustainability and material efficiency among major market priorities. That pressure is real.
However, reducing plastic without testing barrier performance is a weak decision. I have seen attractive packs fail after humid storage. Test samples under actual transport and storage conditions.
Some specifications will need revision. That is better than discovering the weakness after launch.