-
- Products
- Indoor Household Cords
- Appliance Cords
- General Purpose Short-Length Cords
- General Purpose Extension Cords
- Landscape & Decorating Cords
- Bright Color Extension Cords
- Oil-Resistant Extension Cords
- Cold-Flex Extension Cords
- VividFlex Power Cords
- EXTREME All-Weather Cords
- Cord Management
- Task Lights
- Adapters & GFCI Devices
- Where to Buy
- About
- Careers
- Glossary
- Catalog

China Top 10 Stainless Steel Mesh Sheet Manufacturers?
Choosing among China’s top 10 Stainless Steel Mesh Sheet manufacturers requires more than comparing polished websites. Buyers need dependable evidence, practical experience, and clear technical information. A strong supplier should explain wire diameter, aperture size, mesh count, material grade, surface finish, and production tolerance.
This guide examines manufacturers through measurable factors, including factory capability, quality control, export experience, customization support, and customer communication. It also considers whether suppliers provide material certificates, inspection reports, samples, and traceable production records. These details matter. A 304 stainless steel mesh may suit general filtration, while 316 or 316L can offer better resistance in chloride-rich environments. The correct choice depends on the application.
Real projects reveal more than brochures. A buyer may need a tightly woven sheet for laboratory filtration, a rigid panel for screening, or a cut-to-size piece for industrial equipment. Each use requires different strength, opening accuracy, and finishing standards. Packaging also matters when sheets travel long distances. Bent edges or surface contamination can create avoidable losses.
No ranking can fit every purchasing situation. That is worth remembering. Some manufacturers may excel at large-volume orders, while others respond better to prototypes or unusual specifications. This overview therefore focuses on verifiable strengths rather than exaggerated claims. Readers should still request current quotations, samples, compliance documents, and production photographs before placing an order. Careful comparison is slower, but usually safer. Small details often decide whether a mesh sheet performs reliably after installation.
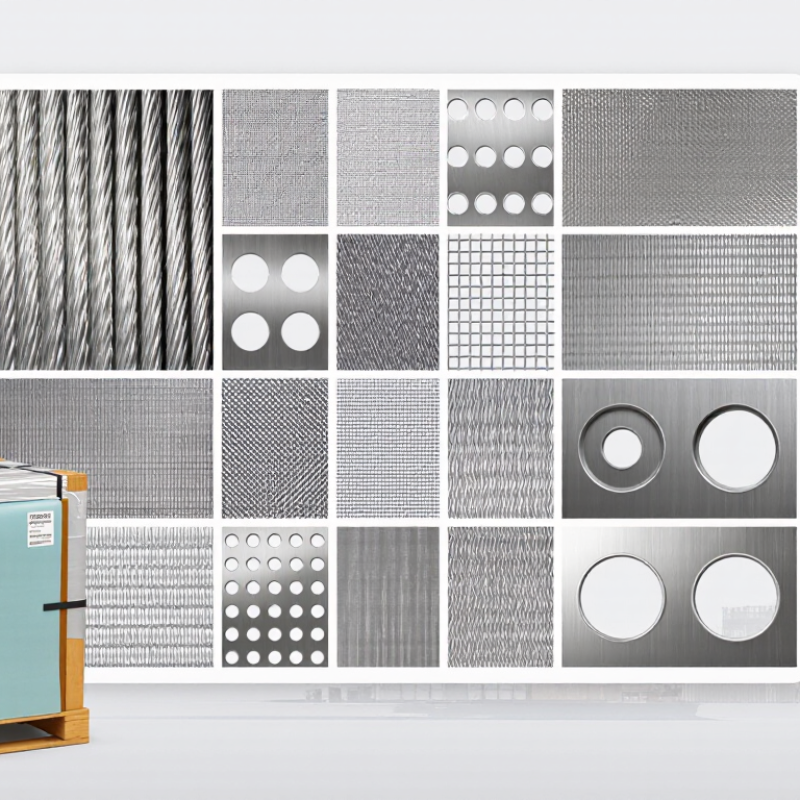
Table of Contents [Hide]
What Is Stainless Steel Mesh Sheet and Where Is It Used?
Stainless steel mesh sheet is a flat metal screen made from corrosion-resistant stainless steel wire. Manufacturers produce it through weaving, welding, or perforating, depending on the required opening pattern. Common grades include 304 and 316, while 316 performs better in chloride-rich environments. Wire diameter and aperture size control filtration accuracy, airflow, strength, and weight. Small openings can trap fine particles, but they may reduce flow noticeably.
The World Stainless Association reported global stainless crude steel production at about 58.4 million tonnes in 2023. This scale supports wide mesh applications across filtration, food processing, chemical equipment, mining, construction, and architectural screens. In practice, stainless mesh sheet can appear inside a liquid filter or across a sunshade façade. It also supports machine guards and drying trays. A 2024 industrial filtration market assessment identified water treatment and process industries as important demand areas. Yet selection is not simply about choosing the finest mesh. Salt exposure, temperature, cleaning chemicals, and mechanical load must be checked together. A common mistake is treating 304 and 316 as interchangeable. They are not. Even a well-made sheet can fail when the opening tolerance or edge treatment is ignored. Supplier samples, material certificates, and dimensional inspection remain valuable when comparing Chinese manufacturers.