-
- Products
- Indoor Household Cords
- Appliance Cords
- General Purpose Short-Length Cords
- General Purpose Extension Cords
- Landscape & Decorating Cords
- Bright Color Extension Cords
- Oil-Resistant Extension Cords
- Cold-Flex Extension Cords
- VividFlex Power Cords
- EXTREME All-Weather Cords
- Cord Management
- Task Lights
- Adapters & GFCI Devices
- Where to Buy
- About
- Careers
- Glossary
- Catalog

How to Choose an Auto Pipe Welding Machine in 2026?
Choosing an Auto Pipe Welding Machine in 2026 requires more than comparing amperage, price, and advertised travel speed. The machine must fit pipe diameter, wall thickness, alloy, joint design, production volume, and site conditions. A workshop welding stainless steel spools needs different control precision than a field crew joining carbon-steel lines. Small details matter, including torch clearance, wire-feeder stability, heat-input control, and how quickly operators can correct arc deviations.
Industry data shows why this decision deserves careful review. The International Federation of Robotics reported 541,302 industrial robots installed worldwide in 2023, confirming broader manufacturing investment in automation. MarketsandMarkets also projects continued growth in the global welding equipment market through 2028. However, these reports cover wider equipment categories, not Auto Pipe Welding machines alone. That distinction matters. Buyers should avoid treating broad market growth as proof that every automated system will improve their operation.
Welding metallurgist John C. Lippold has emphasized a practical principle: “Successful welding depends on controlling the process variables, not simply selecting advanced equipment.” His point remains relevant when comparing orbital systems, robotic manipulators, and integrated pipe stations. A reliable evaluation should examine weld repeatability, documented procedure support, operator training, maintenance access, data logging, and compatibility with qualified welding procedures. Ask for real production samples. Inspect the root profile. Review defect records. The choice is practical.
Some specifications can look impressive on paper but disappoint beside a hot pipe, limited access, or inconsistent fit-up. This guide explains how to compare machines realistically, identify hidden costs, and select equipment that supports safe, repeatable, and auditable welding performance.
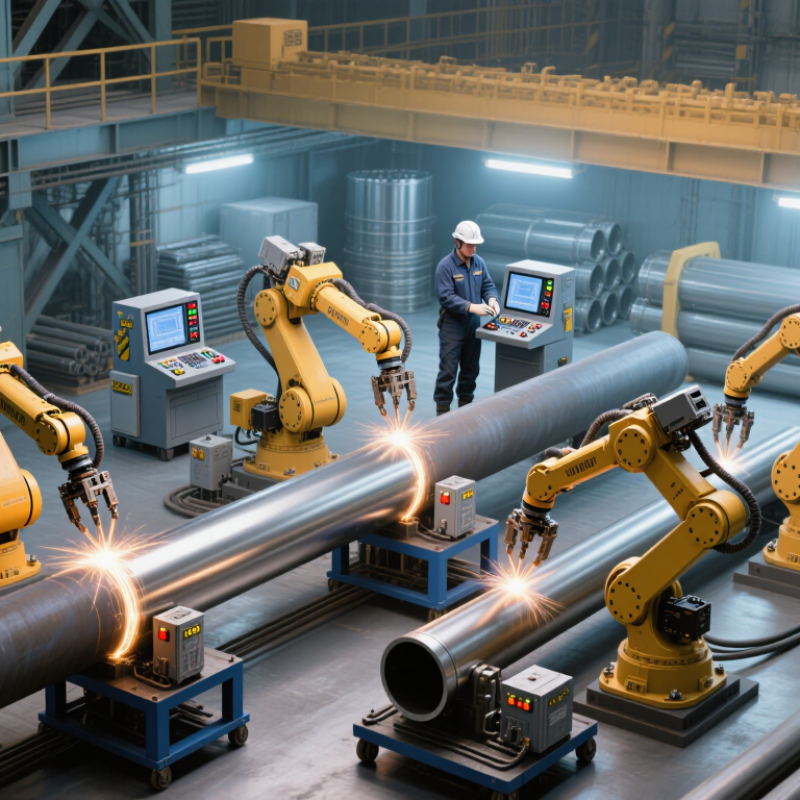
Table of Contents [Hide]
Define Pipe Size, Wall Thickness, and Materials for 2026 Welding Needs
How to Choose an Auto Pipe Welding Machine in 2026?
Pipe size determines machine capacity, clamping range, and torch travel. Record outside diameter, inside diameter, and joint access before comparing equipment. Measure twice. A machine designed for 2-inch pipe may struggle with 24-inch sections. Large-diameter work also needs stronger alignment control and steadier rotation. The International Energy Agency’s World Energy Investment 2024 report expects global energy investment to exceed 3 trillion dollars in 2024. That growth will increase demand for consistent pipeline welding, but project specifications still control the purchase.
Wall thickness affects heat input, pass planning, and welding speed. Thin-wall stainless pipe can burn through under excessive current. Thick carbon-steel walls may require preheating, multiple passes, and slower travel. Select a system that records current, voltage, travel speed, and interpass temperature. ASME Boiler and Pressure Vessel Code Section IX and ISO 15614-1 provide useful qualification frameworks. They do not replace a project-specific welding procedure. That assumption fails.
Material selection matters just as much. The World Steel Association reported about 1.89 billion tonnes of crude steel production in 2023, showing the scale and variety of steel applications. Carbon steel, stainless steel, duplex steel, and nickel alloys require different shielding gases, filler metals, and thermal limits. In field reviews, teams often specify diameter but overlook wall variation. Check the complete thickness range, material certificates, joint design, and allowable heat input. A short trial weld can expose poor fit-up, awkward torch access, or unstable arc behavior before production begins.