-
- Products
- Indoor Household Cords
- Appliance Cords
- General Purpose Short-Length Cords
- General Purpose Extension Cords
- Landscape & Decorating Cords
- Bright Color Extension Cords
- Oil-Resistant Extension Cords
- Cold-Flex Extension Cords
- VividFlex Power Cords
- EXTREME All-Weather Cords
- Cord Management
- Task Lights
- Adapters & GFCI Devices
- Where to Buy
- About
- Careers
- Glossary
- Catalog

How to Choose Petroleum Coke by Composition?
How to Choose Petroleum Coke by Composition?
Choosing petroleum coke starts with composition, not appearance. A shiny black surface can hide high sulfur, metals, or unstable moisture levels. Buyers should examine sulfur, volatile matter, ash, fixed carbon, moisture, vanadium, and nickel. These values affect combustion, emissions, handling, and equipment wear.
Dr. James G. Speight, a recognized petroleum-products authority, states, “The properties of petroleum coke are determined by the feedstock and the coking process.” This principle remains practical at the purchasing stage. Delayed coking conditions can change pore structure, density, and volatile content. Crude oil also leaves a clear chemical fingerprint. Heavy, sour feedstocks often produce coke with higher sulfur and metal concentrations.
Start with the end use. Fuel-grade coke may require controlled sulfur and metal levels. Calcined petroleum coke needs suitable volatile matter and low impurities. Aluminum anode producers usually focus on sulfur, vanadium, nickel, iron, ash, and real density. Small differences matter. A few tenths of a percent can affect furnace behavior or anode performance.
Laboratory data should come from recent, representative samples. Do not rely only on a supplier’s standard sheet. Test cargo-specific material when possible. Review sampling methods, reporting units, and test standards carefully. This is where decisions often become imperfect. One analysis may not represent an entire shipment. Storage can also introduce moisture and handling variation.
The best selection balances chemistry, performance, supply consistency, and total cost. Petroleum Coke Composition is not a single specification. It is a practical risk profile that must match the process.
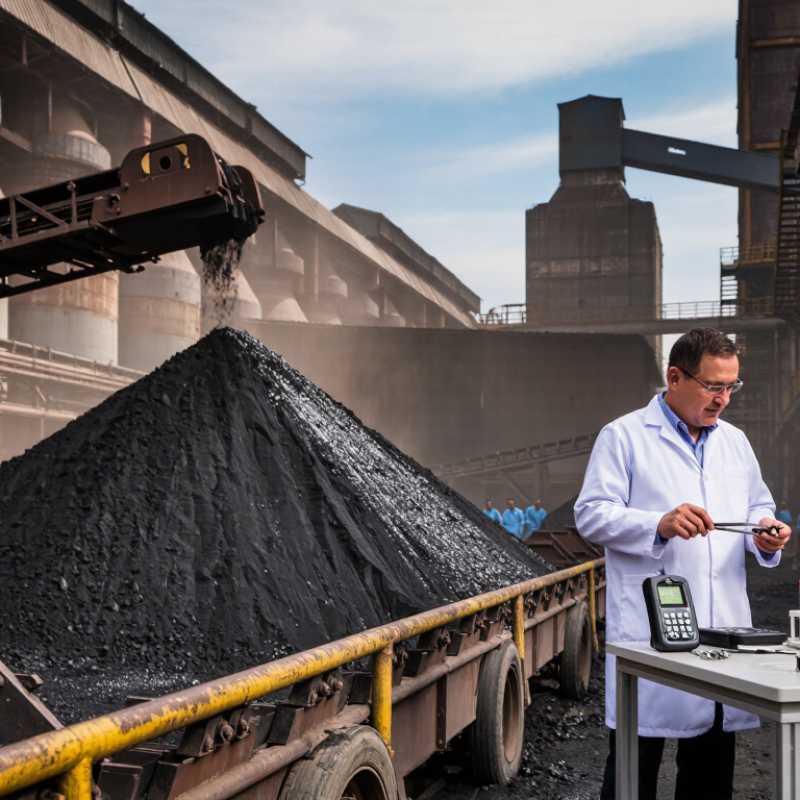
Table of Contents [Hide]
Petroleum Coke Composition: Key Properties and Quality Indicators
Choosing petroleum coke by composition begins with sulfur, volatile matter, ash, moisture, and fixed carbon. These values affect emissions, handling, heat output, and furnace stability. ASTM D4239 measures sulfur, while ASTM D3174 determines ash. ASTM D346 assesses moisture. Use the same methods for every sample.
The U.S. Energy Information Administration reports that petroleum coke remains a significant refinery by-product, but its composition varies with crude feedstock and conversion severity. A practical screening range is 85–92% fixed carbon, 3–12% volatile matter, and 0.2–8% sulfur. These figures are indicative, not universal specifications. The U.S. Geological Survey also identifies vanadium and nickel as important trace elements in petroleum coke trade and processing.
Look beyond the headline carbon number. High ash can increase residue and reduce usable heat. Elevated vanadium may accelerate refractory wear. Moisture above the contract limit adds transport cost and disturbs feeding. A low-sulfur result can still mislead when metals or ash remain high. I would request recent composite samples, not one scoop from the surface. Check laboratory accreditation, test dates, particle size, and basis reporting. Some certificates use air-dried values; others use as-received values. That difference is easy to miss. It can change purchasing decisions. (Sources: EIA International Energy Statistics; USGS Mineral Commodity Summaries 2024; ASTM petroleum coke testing standards.)