-
- Products
- Indoor Household Cords
- Appliance Cords
- General Purpose Short-Length Cords
- General Purpose Extension Cords
- Landscape & Decorating Cords
- Bright Color Extension Cords
- Oil-Resistant Extension Cords
- Cold-Flex Extension Cords
- VividFlex Power Cords
- EXTREME All-Weather Cords
- Cord Management
- Task Lights
- Adapters & GFCI Devices
- Where to Buy
- About
- Careers
- Glossary
- Catalog

How to Choose a Dishwasher Tub Assembly Line?
Choosing a Dishwasher Tub Assembly Line is a production decision, not merely an equipment purchase. The line must shape, weld, inspect, and transfer tubs consistently, even when models change. A stainless-steel tub may look simple, but small dimensional errors can affect sealing, noise control, and final assembly.
Market evidence supports careful planning. Grand View Research estimates that the global dishwasher market was worth about USD 7.8 billion in 2023, with strong growth expected through 2030. Mordor Intelligence also forecasts continued expansion, although its market estimates differ. This variation matters. Demand may grow, but every factory faces different labor costs, product sizes, energy limits, and quality requirements.
Standards matter most.
Taiichi Ohno, the Toyota Production System pioneer, stated, “Without standards, you cannot say, ‘We have improved.’” His principle applies directly to a Dishwasher Tub Assembly Line. Before comparing suppliers, manufacturers should define cycle time, weld strength, leak-test accuracy, changeover time, automation level, and operator safety. The line should also record traceable data from forming through inspection.
A practical review starts with the factory floor. Measure available space. Check material flow. Observe how a tub moves between stations. A crowded transfer area can create hidden delays.
Do not trust impressive speed alone. A faster line may produce more defects if fixtures, sensors, or maintenance systems are weak. That is an easy mistake to make. The better choice balances output, flexibility, energy consumption, after-sales support, and long-term reliability. This guide explains how to compare those factors with greater confidence.
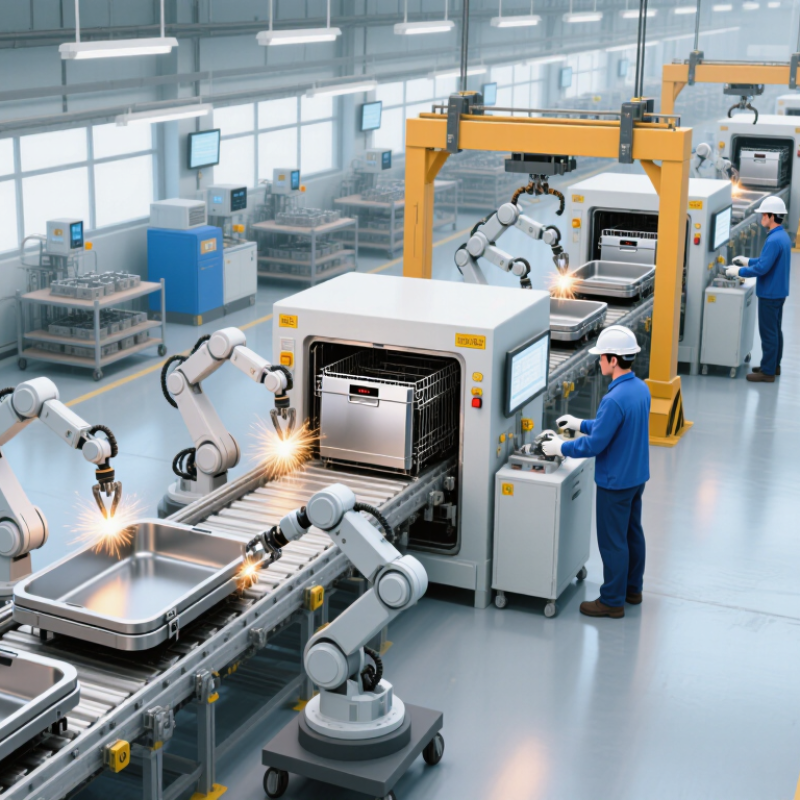
Table of Contents [Hide]
Define Capacity Targets: 10–15 Place Settings and ≤60 dB Noise
How to Choose a Dishwasher Tub Assembly Line?
When choosing a dishwasher tub assembly line, capacity and noise targets should guide every engineering decision. A practical household range is 10–15 place settings per cycle. This range supports compact kitchens and larger family loads. Yet capacity is not only a number. Engineers should test plates, bowls, glasses, and oversized cookware inside real prototypes. A crowded rack may meet specifications but clean poorly. That weakness must be faced early.
Tips: Build a sample tub before finalizing the line. Measure usable volume, rack clearance, spray coverage, and loading speed. Record results from repeated tests, not one impressive run. Measure the tub. Repeat the test. Small errors become expensive after tooling begins.
For noise, set a target of 60 dB or below during complete operation. Test washing, draining, and drying separately, because each stage creates different sounds. Use calibrated instruments in a controlled room. Check vibration at the tub, door, pump, and floor contacts. A quiet prototype can become louder after panels, seals, or fasteners change. This happens more often than teams expect. Line suppliers should provide traceable inspection records and process controls. Review them with production, quality, and service engineers. The best assembly line balances output, repeatability, acoustic control, and repair access. Do not treat the first successful sample as final proof.