-
- Products
- Indoor Household Cords
- Appliance Cords
- General Purpose Short-Length Cords
- General Purpose Extension Cords
- Landscape & Decorating Cords
- Bright Color Extension Cords
- Oil-Resistant Extension Cords
- Cold-Flex Extension Cords
- VividFlex Power Cords
- EXTREME All-Weather Cords
- Cord Management
- Task Lights
- Adapters & GFCI Devices
- Where to Buy
- About
- Careers
- Glossary
- Catalog

How to Choose a Microwave Oven Baffle Die?
Choosing a Microwave Oven Baffle Die is a tooling decision with direct effects on airflow, noise, safety, and production cost. The baffle may look simple, yet its slots, curves, and mounting points must remain consistent across thousands of parts. A small burr can interrupt assembly. A slight dimensional shift can weaken the microwave’s internal air-management performance.
Industry reports show why this choice deserves careful evaluation. The International Energy Agency’s Energy Efficiency Market Report highlights continuing pressure to reduce appliance energy use and improve manufacturing efficiency. Meanwhile, market analyses from Grand View Research and Fortune Business Insights describe steady global demand for microwave ovens, especially in compact household and built-in segments. These trends increase the need for durable, repeatable tooling. A die that performs well during trials may still fail under long production cycles. That uncomfortable possibility matters.
This guide examines die material, forming method, tolerance control, surface treatment, maintenance access, and supplier capability. It also considers IEC 60705, which provides internationally recognized methods for testing household microwave oven performance. The standard does not select a die for you, but it clarifies why stable component geometry matters. Look closely at edge quality and springback. Check sample parts under actual assembly conditions. Ask for measurable evidence, not attractive promises. Production reality is less forgiving.
The right Microwave Oven Baffle Die should deliver consistent parts, manageable maintenance, and predictable service life. Price alone is not enough. A cheaper die can become expensive through scrap, rework, and delayed delivery. Choose with data. Recheck assumptions.
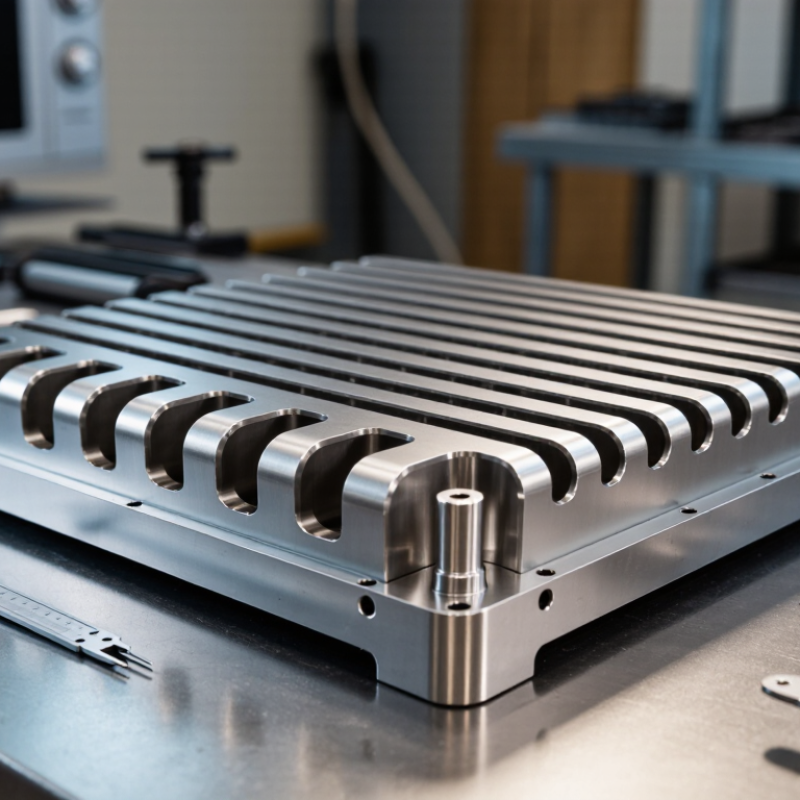
Table of Contents [Hide]
Microwave Oven Baffle Dies: Purpose, Structure, and Working Principles
How to Choose a Microwave Oven Baffle Die?
A microwave oven baffle die forms thin metal parts that redirect airflow or control internal microwave distribution. Its accuracy affects heating consistency, noise, and assembly fit. A practical die usually includes an upper shoe, lower shoe, punch, die plate, guide pillars, stripper, and ejector pins. The baffle may also require lancing, bending, or shallow drawing. Each operation changes the die layout.
The working principle is direct. A press drives the punch into the sheet, while the die supports and shapes the material. Correct clearance limits burrs and prevents torn edges. For stainless steel, engineers often begin with clearance near 6% to 10% of sheet thickness, then confirm it through trials. Springback still causes trouble. I have seen a seemingly accurate bend open slightly after unloading.
Choose the die after checking material grade, thickness, annual volume, and required tolerance. Progressive dies suit stable, high-volume production. Compound dies can combine blanking and piercing in one stroke. For lower volumes, a simpler single-operation die may reduce maintenance risk. The 2024 Grand View Research report estimated the global microwave oven market at over USD 10 billion, showing why repeatable tooling matters. Meanwhile, the World Tooling Report links tighter stamping control with lower scrap, although its figures vary by region. Do not trust reports blindly. Validate them against your press tonnage, coil quality, and first-article measurements. A polished die is not automatically a reliable die.