-
- Products
- Indoor Household Cords
- Appliance Cords
- General Purpose Short-Length Cords
- General Purpose Extension Cords
- Landscape & Decorating Cords
- Bright Color Extension Cords
- Oil-Resistant Extension Cords
- Cold-Flex Extension Cords
- VividFlex Power Cords
- EXTREME All-Weather Cords
- Cord Management
- Task Lights
- Adapters & GFCI Devices
- Where to Buy
- About
- Careers
- Glossary
- Catalog

What Is a Dicing Machine and How Does It Work?
A Dicing Machine is a precision cutting system used to separate wafers, panels, and other fragile materials into smaller units. It appears in semiconductor, electronics, ceramics, glass, and medical-device production. The machine may look compact, yet every movement matters.
A typical Dicing Machine holds the workpiece on a vacuum table. A diamond blade spins at high speed and follows programmed cutting paths. Coolant carries away heat and loose particles. The operator adjusts spindle speed, feed rate, blade exposure, and cutting depth. These settings affect kerf width, edge chipping, surface damage, and production time. One small error can ruin several useful components.
Dr. Chris A. Mack, a respected semiconductor manufacturing educator, has emphasized a practical truth: “A process is only good when it is repeatable.” That principle explains why dicing requires more than a sharp blade. The machine must maintain alignment, vibration control, cooling, and stable workholding throughout the cycle. Experienced technicians inspect cut edges under magnification, not only the machine display.
Still, no universal setting exists. Different materials respond differently. Silicon, glass, ceramic, and composite panels may require separate blades and cutting strategies. A faster feed rate can improve output, but it may increase chipping. A slower cut can look cleaner, yet it may raise cost and heat exposure. Even a well-designed process deserves review. This guide examines what a Dicing Machine is, how its main systems work, and why practical adjustments often decide the final quality.
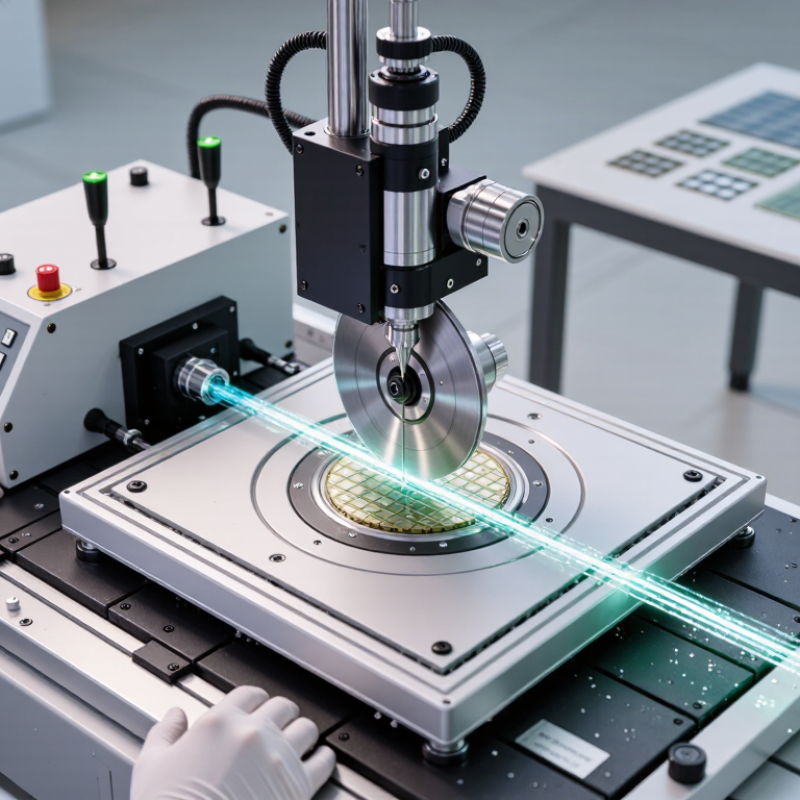
Table of Contents [Hide]
What Is a Dicing Machine?
What Is a Dicing Machine?
A dicing machine is equipment that cuts food into consistent cubes or rectangular pieces. It is commonly used for vegetables, fruits, cheese, cooked meat, and other firm ingredients. Unlike hand cutting, it can produce hundreds of similar pieces within a short period. This consistency supports even cooking, accurate portioning, and cleaner food presentation.
A typical machine includes a product hopper, feeding system, cutting blades, and an exit chute. An operator places prepared food into the hopper. The feeding system pushes it toward a set of sharp blades. One blade or grid makes strips, while another cuts those strips into cubes. Size settings can often be adjusted by changing the cutting grid or feed speed. Small details matter. A softer tomato may need slower feeding, while a firm potato may require stronger pressure.
In practice, the machine does not remove every production challenge. Uneven ingredients can create irregular pieces, and blunt blades may crush rather than cut. Moisture, temperature, and product shape also affect results. Operators should inspect the cutting chamber, clean food-contact surfaces, and follow the equipment manual before use. Safety guards must remain in place during operation. A short trial batch is useful. It reveals problems before large quantities are processed. Even experienced workers may need to adjust settings when ingredients change during the day.