-
- Products
- Indoor Household Cords
- Appliance Cords
- General Purpose Short-Length Cords
- General Purpose Extension Cords
- Landscape & Decorating Cords
- Bright Color Extension Cords
- Oil-Resistant Extension Cords
- Cold-Flex Extension Cords
- VividFlex Power Cords
- EXTREME All-Weather Cords
- Cord Management
- Task Lights
- Adapters & GFCI Devices
- Where to Buy
- About
- Careers
- Glossary
- Catalog

10 Tips for Buying Mild Steel Pipe Worldwide
Buying Mild Steel Pipe across borders looks simple until the first shipment arrives. A drawing may show diameter and wall thickness, yet the real decision includes steel grade, manufacturing method, surface condition, tolerances, testing, and documentation. One small mismatch can delay installation beside a busy construction site.
John Packard, a recognized steel-market analyst, has stated, “Price is only one part of the pipe-buying decision.” That point deserves attention. A low quotation may hide weak traceability, unclear standards, or expensive inland transport. Cheap is not always economical.
This guide presents ten practical tips for purchasing Mild Steel Pipe worldwide. It considers supplier experience, mill test certificates, inspection procedures, packaging, payment terms, and delivery planning. Buyers should compare equivalent specifications, not isolated numbers. A pipe priced per ton may appear attractive, while cutting losses and freight change the final cost.
Details matter. Confirm whether dimensions follow ASTM, EN, API, or another required standard. Check whether the pipe is welded or seamless. Ask how bundles will be protected from rain, salt air, and forklift damage. Request recent test records, but do not treat paperwork as proof by itself.
No checklist is perfect. I may still miss a regional requirement or an unusual project condition. That is why careful questioning remains valuable. The strongest purchase combines verified quality, clear communication, realistic logistics, and a supplier willing to explain uncomfortable details before production begins.
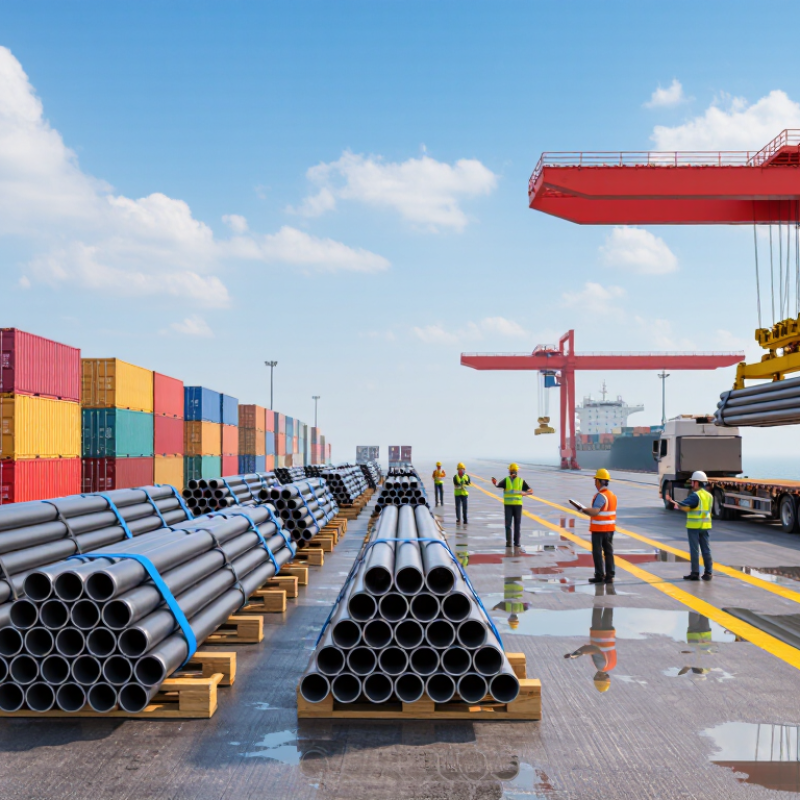
Table of Contents [Hide]
Define Mild Steel Pipe Specifications and Intended Applications
Define mild steel pipe specifications before comparing prices. Mild steel usually means low-carbon steel, but the term is not a complete purchasing standard. State the outside diameter, wall thickness, length tolerance, steel grade, end finish, and test requirements. A 168.3 mm outside diameter pipe with a 6.3 mm wall behaves differently from a thinner irrigation pipe. Intended use controls the choice. Water lines may require corrosion protection and clean internal surfaces. Structural frames need dimensional accuracy and load calculations. Compressed-air or process lines need pressure ratings, weld quality, and documented testing.
Standards reduce ambiguity across borders. ASTM A53 commonly covers general-purpose pipe, while ASTM A106 addresses seamless carbon steel pipe for elevated-temperature service. EN 10219 is often relevant to cold-formed structural hollow sections. Confirm the applicable edition with an engineer. ISO 3183 may apply to pipeline transportation systems, but it is not automatically suitable for every project. The World Steel Association reported approximately 1.89 billion tonnes of crude steel production in 2023, showing the scale of the supply chain, not uniform quality. Ask for a mill test certificate, heat number, chemical composition, tensile results, and hydrostatic test records. Measure random pieces with a calibrated caliper. I once underestimated coating thickness; the usable internal diameter was smaller than expected. That detail matters. Recheck it.
| No. | Buying Dimension | Recommended Specification or Data | Typical Options | Suitable Applications | Important Verification Point |
|---|---|---|---|---|---|
| 1 | Pipe Material | Low-carbon, non-alloy carbon steel commonly referred to as mild steel. The exact chemical composition must be confirmed against the selected standard. | Carbon content is generally controlled at a low level to support formability and weldability; limits vary by standard and grade. | Water lines, structural work, compressed-air systems, general fabrication, and low-to-moderate temperature service. | Do not rely on the term “mild steel” alone. Request the material grade, chemical composition, mechanical properties, and test certificate. |
| 2 | Applicable Standard | Select a standard based on the service, country, and project specification. | ASTM A53 for general mechanical and pressure applications; ASTM A106 for seamless pipe at elevated temperatures; API 5L for pipeline service; EN 10255 for screwed or plain-end tubes; EN 10217-1 for welded pressure purposes. | Building services, process piping, oil and gas transmission, water distribution, and industrial piping. | Confirm the latest project-approved edition, conformity requirements, inspection level, and marking rules before ordering. |
| 3 | Grade Selection | Choose a grade according to required yield strength, tensile strength, weldability, temperature, and pressure conditions. | ASTM A53 Grade B; ASTM A106 Grade B; API 5L Grade B; EN 10255 S195T; EN 10217-1 P195TR1 or P235TR1, subject to the applicable product standard. | Grade B products are widely used for general carbon-steel piping; European grades may be selected where EN standards apply. | Equivalent grades are not automatically interchangeable. Compare the complete standard, dimensions, testing, and delivery condition. |
| 4 | Manufacturing Process | Specify whether the pipe is seamless or welded, and state the required forming or heat-treatment condition. | Seamless; electric-resistance welded; longitudinally welded; hot-finished; cold-drawn, where permitted by the standard. | Seamless pipe is often selected for demanding temperature or pressure service; welded pipe is commonly used for general piping and structural applications. | Manufacturing route affects cost, dimensional range, inspection, and suitability. It does not replace the need to verify the applicable standard. |
| 5 | Nominal Size and Outside Diameter | Define nominal pipe size or outside diameter together with the governing dimensional standard. | Common nominal sizes include DN25, DN50, DN100, and DN200; common NPS equivalents include NPS 1, 2, 4, and 8. | Process piping, water systems, fire-protection systems, structural columns, handrails, and fabricated assemblies. | DN and NPS designations are nominal references and should not be treated as exact outside-diameter measurements without checking the standard. |
| 6 | Wall Thickness | Specify wall thickness directly or identify the required schedule, mass series, or thickness class. | Schedule 10, Schedule 40, Schedule 80, or a project-defined thickness; EN 10255 medium and heavy series where applicable. | Light-duty utilities may use thinner walls, while pressure, impact, corrosion allowance, or structural loads may require thicker walls. | Calculate pressure design thickness using the applicable code. Include corrosion allowance, manufacturing tolerance, and threading allowance where relevant. |
| 7 | Pipe Ends and Connection | Define the required end configuration and connection method. | Plain ends, beveled ends for butt welding, threaded ends, grooved ends, or flanged ends. | Welded process lines, threaded utility piping, grooved fire-protection systems, and flanged equipment connections. | For threaded pipe, verify thread type and length. For butt-welded pipe, confirm bevel angle, root face, and end protection requirements. |
| 8 | Length and Dimensional Tolerance | State random length, fixed length, permitted outside-diameter tolerance, wall-thickness tolerance, straightness, and ovality requirements. | Random lengths are commonly supplied for stock piping; fixed lengths are used for fabrication and installation control. | Infrastructure projects, prefabricated modules, structural frames, and production lines with controlled cut lengths. | Actual tolerances depend on the product standard. Request the dimensional inspection report when tight fit-up is important. |
| 9 | Surface Protection | Choose the finish according to exposure, storage period, transport conditions, and corrosion risk. | Black bare finish, oiled finish, externally galvanized coating, painted coating, or project-specified anti-corrosion system. | Indoor fabrication, outdoor structures, water service, temporary protection during shipment, and corrosive environments. | Galvanizing thickness, coating adhesion, repair method, and inspection criteria should be specified separately from the steel grade. |
| 10 | Inspection, Documents, and Logistics | Define testing, documentation, packing, marking, delivery terms, and destination requirements before purchase. | Heat number marking, mill test certificate, chemical analysis, tensile test, bend or flattening test, hydrostatic or nondestructive testing where required, and third-party inspection. | International procurement, regulated projects, pressure systems, pipeline construction, and quality-controlled fabrication. | Confirm certificate type, traceability, inspection scope, packaging, Incoterms, port requirements, customs documents, and local compliance obligations. |