-
- Products
- Indoor Household Cords
- Appliance Cords
- General Purpose Short-Length Cords
- General Purpose Extension Cords
- Landscape & Decorating Cords
- Bright Color Extension Cords
- Oil-Resistant Extension Cords
- Cold-Flex Extension Cords
- VividFlex Power Cords
- EXTREME All-Weather Cords
- Cord Management
- Task Lights
- Adapters & GFCI Devices
- Where to Buy
- About
- Careers
- Glossary
- Catalog

How to Choose the Right Palletizing Machine?
Choosing the right Palletizing Machine is not simply a matter of selecting the fastest model. The decision begins with the product, the pallet, and the people operating the line. Bags of flour behave differently from rigid cartons. Fragile bottles need softer handling and controlled acceleration. Heavy cases demand accurate gripping, stable stacking, and reliable pallet support.
Roberto Michel, an experienced materials-handling analyst, has offered a useful principle: “The best automation projects begin with a clear understanding of the process.” That advice matters when reviewing pallet patterns, case dimensions, product weight, line speed, and available floor space. A machine rated for 1,200 cases per hour may disappoint if carton sizes change frequently. Flexibility can matter more than maximum speed. Sometimes, less is better.
A practical evaluation should include gripper selection, conveyor integration, safety access, changeover time, maintenance support, and future production needs. Ask the supplier to demonstrate your actual cartons, not a similar-looking sample. Watch the machine build a complete pallet. Check corner alignment, layer stability, and film-wrapping performance. Review factory acceptance testing and service response times before signing an agreement.
No Palletizing Machine fits every factory perfectly. That is the uncomfortable part. Forecasts can be wrong, packaging may change, and operators may resist unfamiliar controls. A thoughtful choice leaves room for these weaknesses. It balances measurable output with daily usability, dependable engineering, and evidence from real production conditions.
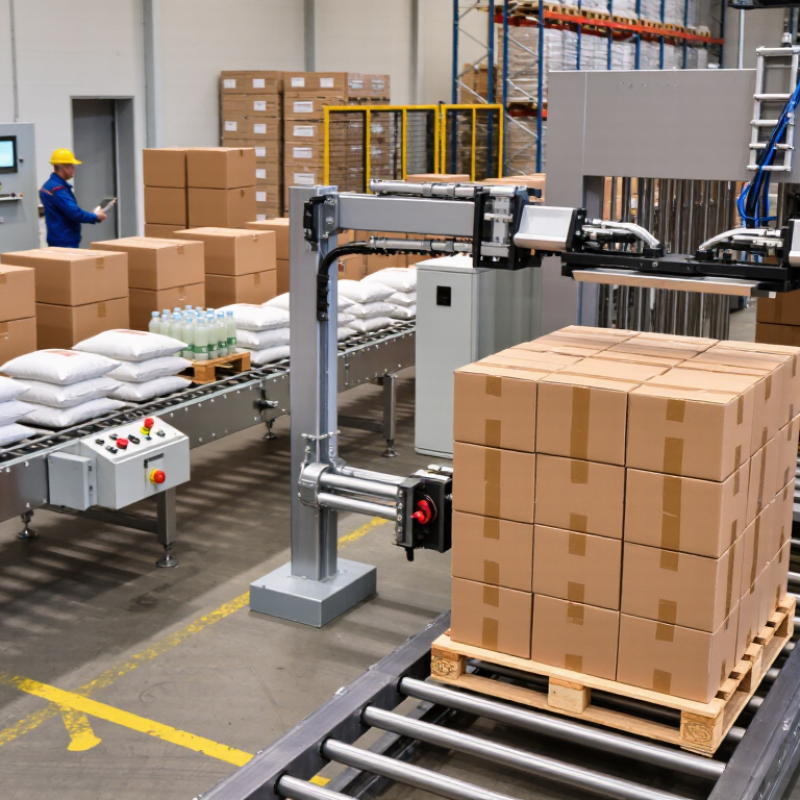
Table of Contents [Hide]
Define Your Palletizing Requirements and Production Goals
A practical choice starts with a clear production profile, not a machine brochure. Record current output by hour, shift, and season. Include carton dimensions, product weight, pallet size, and stacking pattern. Note changes too. A line making 20 cases per minute today may need 30 next year. That gap affects gripper design, robot reach, and cycle time.
Walk the production floor with an operator and maintenance technician. Measure conveyor height, available space, pallet access, and forklift paths. Check whether cases arrive square, sealed, and consistently spaced. Small variations can create repeated jams. Define acceptable downtime, changeover time, and operator involvement. If products are fragile, dusty, cold, or irregular, document those conditions before requesting quotations. Real production rarely matches a clean specification sheet.
Set goals that can be tested. For example, target 95% line availability, a ten-minute pattern change, or reduced manual lifting per shift. Ask suppliers to demonstrate these targets using your actual cases and pallets. Request data on speed at full load, not empty-cycle performance. Review guarding, emergency stops, training, spare parts, and maintenance access against applicable local requirements. I would also challenge optimistic forecasts. Our first estimates are often too generous. Leave room for seasonal demand, product variation, and learning time. A useful specification includes what the machine must do, and what it must never compromise.