-
- Products
- Indoor Household Cords
- Appliance Cords
- General Purpose Short-Length Cords
- General Purpose Extension Cords
- Landscape & Decorating Cords
- Bright Color Extension Cords
- Oil-Resistant Extension Cords
- Cold-Flex Extension Cords
- VividFlex Power Cords
- EXTREME All-Weather Cords
- Cord Management
- Task Lights
- Adapters & GFCI Devices
- Where to Buy
- About
- Careers
- Glossary
- Catalog

How to Bend WPC Boards Safely?
Bend Wpc safely requires more than applying heat and forcing a board into shape. Wood-plastic composite behaves differently from solid wood, PVC, and ordinary decking. Its plastic content softens gradually, while its wood fibers can scorch, split, or permanently weaken. A safe method begins with the manufacturer’s bending limits, board profile, moisture condition, and recommended temperature range.
Daniel Harper, a WPC fabrication specialist, offers a practical reminder: “A smooth curve is useful only when the board keeps its strength afterward.” That principle guides this article. Bend Wpc projects should use controlled heat, steady support, and a generous bending radius. A heat gun can create hot spots, so move it continuously across the surface. Never hold it close to one area for too long. The surface may look acceptable while the inner layers deform.
Wear heat-resistant gloves, eye protection, and suitable clothing. Work in a ventilated area, away from combustible materials. Secure the board with a form or jig before heating it. Apply pressure slowly. Sudden force can produce white stress marks, cracks, or spring-back. Hollow boards need special caution because their internal webs may collapse.
A small test piece is wise. It reveals timing, flexibility, and surface changes before valuable material is used. Even careful work can fail. I would not call any bending method foolproof, especially when board formulas vary between manufacturers. Let the shaped board cool completely before removing supports. Then inspect the curve, edges, and fastening zones for hidden damage.
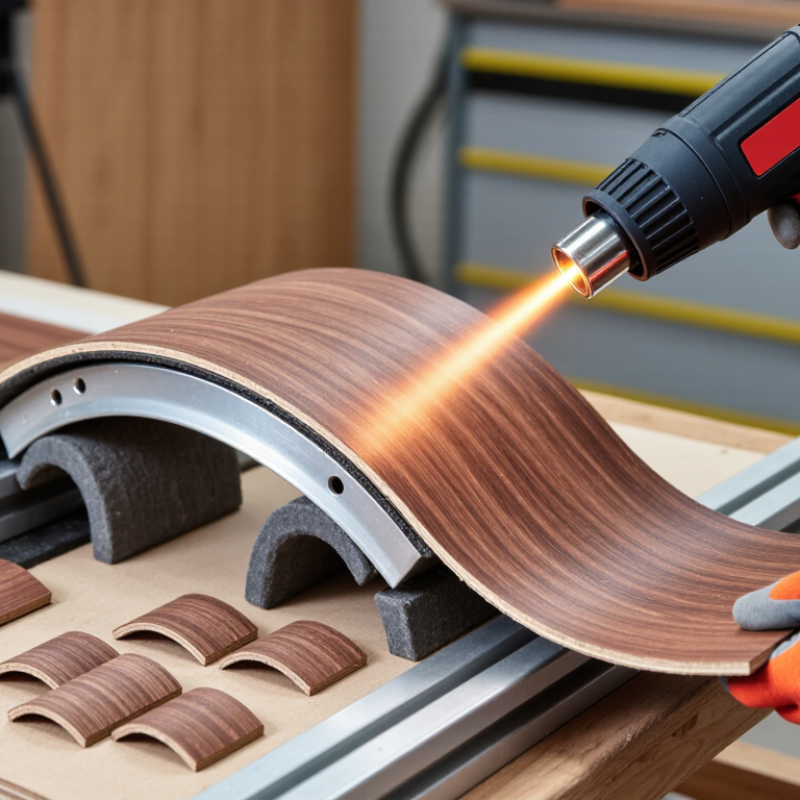
Table of Contents [Hide]
Identify Resin Type, Thickness, and ASTM D790 Flexural Data
How to Bend WPC Boards Safely?
Bending a WPC board starts with identifying its resin type. Thermoplastic WPC can soften under controlled heat, while thermoset material may crack instead. Check the technical sheet, not just the surface appearance. Resin content also affects stiffness, heat response, and recovery after bending. A board with recycled fillers may behave less consistently.
Thickness changes the bending risk dramatically. A 6 mm board may form around a modest curve, but a 20 mm board needs much more heat and force. Measure the intended radius and test a small offcut first. Warm the board evenly, using temperature monitoring rather than guesswork. Protect your hands and keep the material supported. Never force a cold board. It can split internally before damage becomes visible.
ASTM D790 flexural data provides useful evidence for comparison. Flexural modulus indicates resistance to bending, while flexural strength shows the load limit during testing. Flexural strain helps estimate how much deformation the specimen tolerated. However, ASTM D790 results do not guarantee performance in a heated, curved installation. Test conditions, specimen direction, moisture, and thickness all matter.
WPC boards can also show surface whitening after forming. That may signal stress, not merely a cosmetic defect. In my experience, the first sample often looks acceptable but relaxes overnight. I now inspect it again after 24 hours. That extra check has prevented rushed decisions, although it cannot replace project-specific testing.