-
- Products
- Indoor Household Cords
- Appliance Cords
- General Purpose Short-Length Cords
- General Purpose Extension Cords
- Landscape & Decorating Cords
- Bright Color Extension Cords
- Oil-Resistant Extension Cords
- Cold-Flex Extension Cords
- VividFlex Power Cords
- EXTREME All-Weather Cords
- Cord Management
- Task Lights
- Adapters & GFCI Devices
- Where to Buy
- About
- Careers
- Glossary
- Catalog

Top Sludge Dewatering Equipment Manufacturers Worldwide
Sludge dewatering is no longer a minor step behind the treatment plant. It directly affects hauling costs, disposal volume, energy use, and the reliability of wastewater operations. According to the UN-Water SDG 6 Synthesis Report 2023, 42% of household wastewater worldwide was not safely treated in 2022. This gap creates sustained demand for efficient sludge management and dependable dewatering systems.
The Water Environment Federation’s Manual of Practice No. 8 identifies centrifuges, belt filter presses, and screw presses as established technologies for reducing sludge volume. Each option behaves differently beside a real clarifier. A centrifuge may deliver consistent cake dryness, while a belt press can offer simpler visual monitoring. Screw presses often attract smaller facilities because of their lower operating complexity. The European Commission’s Best Available Techniques Reference Document for Waste Treatment also emphasizes energy use, emissions control, maintenance, and process optimization.
The stakes are practical. A few percentage points of solids content can change truck frequency and disposal expense. Yet, manufacturer rankings should not rely on product brochures alone. This guide evaluates Top Sludge Dewatering Equipment Manufacturers Worldwide through equipment performance, application experience, service coverage, automation, lifecycle cost, and documented customer results. Data remains uneven. Some suppliers publish detailed test results, while others provide limited field evidence. That limitation deserves attention, because laboratory performance can differ sharply from sludge containing grit, grease, or seasonal industrial loads. The most credible manufacturers therefore combine proven machinery with pilot testing, responsive technical support, and transparent operating data. This comparison aims to help engineers, contractors, and plant owners make decisions grounded in measurable performance rather than market visibility alone.
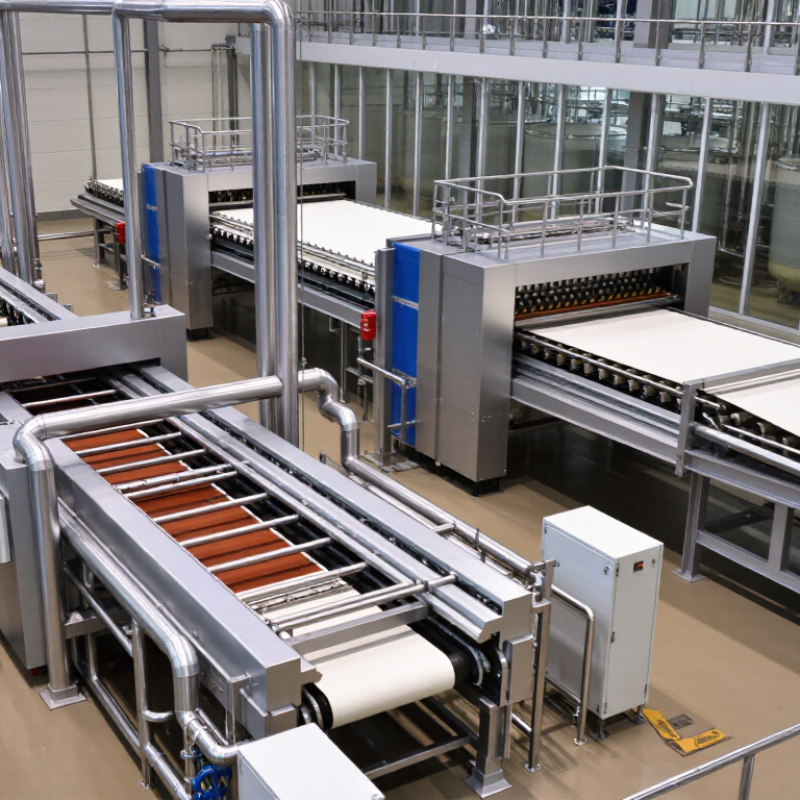
Table of Contents [Hide]
Sludge Dewatering Equipment: Purpose, Principles, and Main Technologies
Top Sludge Dewatering Equipment Manufacturers Worldwide
Sludge dewatering removes free water before hauling, drying, or beneficial reuse. It lowers volume, storage demand, and transport frequency. U.S. Environmental Protection Agency process guidance commonly reports feed sludge at 1–4% solids and dewatered cake at roughly 15–30%. Actual results depend on polymer selection, temperature, and sludge age.
The operating principle is simple. Mechanical force separates water from concentrated solids. Belt filter presses use gravity drainage and compression. Screw presses apply gradual pressure through a rotating shaft. Centrifuges generate high centrifugal force inside a bowl. Filter presses use repeated pressure cycles and can produce drier cakes, but they usually require more labor and batch handling.
The choice should match the sludge, not the brochure. Municipal waste activated sludge often needs careful conditioning before pressing. Industrial sludge may contain abrasive minerals or unusual chemicals. The United Nations World Water Development Report has estimated that more than 80% of global wastewater is discharged without adequate treatment, increasing pressure on treatment capacity. That figure does not determine equipment demand directly, but it shows the scale of the problem.
Field experience remains important. A clean pilot test can mislead. Seasonal sludge changes may reduce capture rates, while excessive polymer can raise operating costs and complicate reuse. Engineers should compare solids capture, cake dryness, power use, wash-water demand, noise, and maintenance access. The best system is rarely the driest one. Reliability matters more than impressive laboratory numbers.