-
- Products
- Indoor Household Cords
- Appliance Cords
- General Purpose Short-Length Cords
- General Purpose Extension Cords
- Landscape & Decorating Cords
- Bright Color Extension Cords
- Oil-Resistant Extension Cords
- Cold-Flex Extension Cords
- VividFlex Power Cords
- EXTREME All-Weather Cords
- Cord Management
- Task Lights
- Adapters & GFCI Devices
- Where to Buy
- About
- Careers
- Glossary
- Catalog

7 Tips for Buying Milling Machinery from Global Suppliers
Buying Milling Machinery from global suppliers is no longer a simple price comparison. It involves engineering fit, supplier reliability, compliance, logistics, and long-term maintenance. Fortune Business Insights reports that the global machine tools market reached approximately USD 84.4 billion in 2023. Its forecast also indicates continued growth through 2032. This broader market includes milling systems, turning equipment, and other precision technologies.
That growth creates more choices, but also more uncertainty. A machine may look impressive in a video yet fail basic production tests. Check spindle speed, taper type, table travel, positioning accuracy, controller compatibility, and coolant capacity. Ask for documented test results. Request a factory acceptance test using material similar to your own workpieces. Small details matter. A poorly protected control cabinet can suffer during sea transport. A missing spare-parts list can delay production for weeks.
The International Trade Centre’s Trade Map shows the complexity of international machinery trade through varied export markets and product classifications. Buyers should therefore verify the supplier’s legal entity, technical certificates, warranty terms, and after-sales capacity. ISO 9001 certification can support process confidence, but it does not guarantee machine performance. CE marking may apply in relevant markets, while other regions may require different conformity procedures. Do not assume one certificate covers every destination. In practice, some purchasing teams still focus too heavily on the initial quotation. That is understandable, but incomplete. A cheaper Milling Machinery package may become expensive after installation, training, tooling, and downtime. These seven tips provide a practical framework for comparing suppliers more carefully and questioning attractive offers before signing.
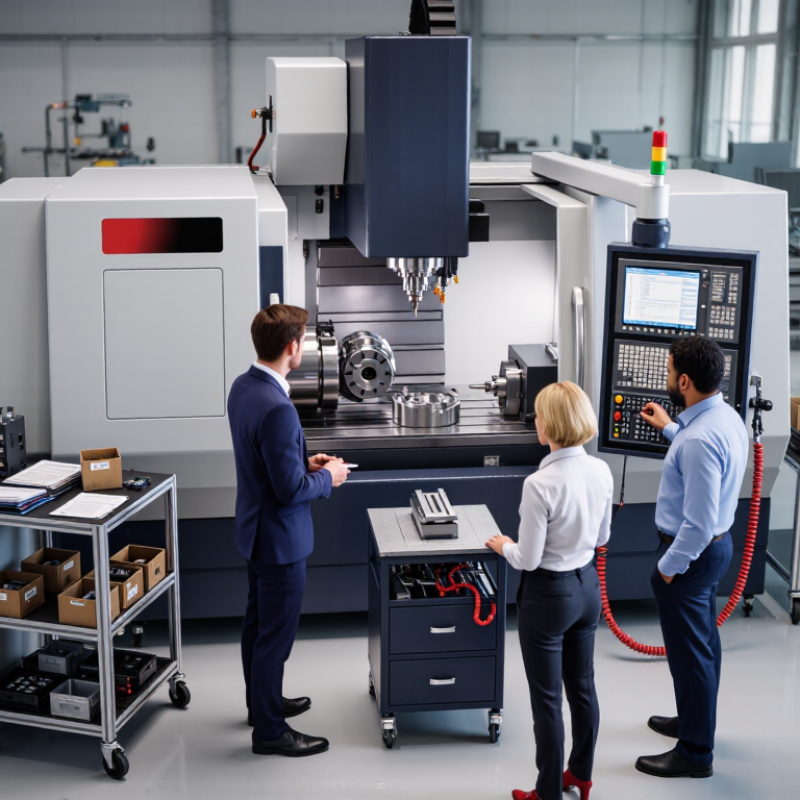
Table of Contents [Hide]
Define Your Milling Requirements and Production Goals
Before contacting global milling machinery suppliers, write down what your production must achieve. Define material, part dimensions, tolerance, surface finish, and target output. Include current bottlenecks, not only ideal plans. A machine that cuts quickly may still fail if setup changes consume half the shift. Measure actual spindle hours, tool changes, scrap rates, and operator loading for several weeks. Small details matter.
I once helped review a purchase based on maximum cutting speed. The team later discovered its parts required stable low-speed torque and frequent fixture changes. That assumption was wrong. Set practical production goals: pieces per hour, monthly volume, acceptable downtime, and payback expectations. Separate essential specifications from desirable upgrades. This makes supplier quotations easier to compare and reduces vague promises. Ask for test-cut evidence using comparable material, tooling, and tolerances. Request cycle-time calculations that include loading, inspection, and tool changes.
Your requirements should reflect future work, but avoid paying for capacity without credible demand. Check floor space, electrical supply, coolant handling, lifting access, training time, and maintenance skills. These constraints often decide whether a technically excellent machine performs well. Leave room for uncertainty. Forecasts can be optimistic, and my early estimates have sometimes been too generous. Review them with operators and maintenance staff before sending a formal inquiry. A clear requirement sheet gives suppliers a reliable basis for configuration, delivery planning, and service support.
7 Tips for Buying Milling Machinery from Global Suppliers - Define Your Milling Requirements and Production Goals
| Tip | Requirement Dimension | Typical Production Target | Suitable Milling Configuration | Key Technical Data to Request | Acceptance Metric |
|---|---|---|---|---|---|
| 1 | Define the workpiece material and hardness | Process aluminum, mild steel, stainless steel, cast iron, or hardened steel consistently | Three-axis machining center for general work; four- or five-axis configuration for complex surfaces | Maximum material hardness, spindle speed range, spindle power, taper type, coolant capability, and recommended cutting parameters | Stable cutting without excessive vibration, burning, chatter, or abnormal tool wear |
| 2 | Set the required part size and working envelope | Machine the largest planned component with adequate clearance for fixtures and tools | Select table size and axis travel at least 10–20% greater than the largest routine workpiece requirement | X/Y/Z travel, table length and width, maximum workpiece weight, spindle-to-table distance, and door opening | Complete access to all machining areas without collisions or repeated repositioning |
| 3 | Match accuracy and surface-finish requirements | General production: approximately ±0.02–0.05 mm; precision work: approximately ±0.005–0.02 mm, depending on process conditions | Precision linear guides, rigid casting, thermal compensation, and high-resolution feedback systems for tighter tolerances | Positioning accuracy, repeatability, ball-screw pitch accuracy, thermal compensation, and spindle runout | Supplier test-cut report, measured dimensional results, and surface roughness value such as Ra in micrometers |
| 4 | Calculate required output and cycle time | For example, 20–100 parts per shift, depending on part complexity, material removal, inspection, and loading time | High-speed spindle and automatic tool changer for short cycles; pallet or automated loading for higher-volume production | Spindle speed, rated power, torque curve, rapid traverse, tool-change time, chip-to-chip time, and estimated cycle time | Verified cycle time per acceptable part, including tool changes, workholding, loading, and inspection |
| 5 | Choose the correct spindle and tooling capacity | Support roughing, semi-finishing, and finishing operations without exceeding spindle torque or tool limits | Medium-speed, high-torque spindle for steel and cast iron; higher-speed spindle for aluminum and small tools | Spindle speed range, continuous and peak power, maximum torque, tool magazine capacity, maximum tool diameter, and tool length | No spindle overload alarms; consistent tool life and cutting performance at planned feed rates |
| 6 | Evaluate automation and operator requirements | Reduce non-cutting time, manual handling, and setup variation while maintaining safe operation | Automatic tool measurement, probing, chip conveyor, mist or flood coolant, and optional pallet or robot interface | Setup time, loading method, probing cycle, chip-removal capacity, control interface, safety functions, and operator training needs | Lower setup time, reduced handling errors, documented safety checks, and clear maintenance procedures |
| 7 | Compare total ownership cost and supplier support | Achieve predictable availability over the planned service life, commonly 10 years or more with proper maintenance | Select a machine with accessible service points, standard consumables, remote diagnostics, and documented preventive maintenance | Purchase price, installation, shipping, electrical requirements, energy use, warranty duration, spare-parts lead time, and service response time | Documented five-year cost estimate, agreed response times, available manuals, and confirmed commissioning plan |
Planning note: Capacity, accuracy, cycle time, tool life, and energy consumption depend on the material, workpiece geometry, cutting tools, fixtures, programming strategy, and operating environment. Request a documented test cut using representative parts before placing the final order.