-
- Products
- Indoor Household Cords
- Appliance Cords
- General Purpose Short-Length Cords
- General Purpose Extension Cords
- Landscape & Decorating Cords
- Bright Color Extension Cords
- Oil-Resistant Extension Cords
- Cold-Flex Extension Cords
- VividFlex Power Cords
- EXTREME All-Weather Cords
- Cord Management
- Task Lights
- Adapters & GFCI Devices
- Where to Buy
- About
- Careers
- Glossary
- Catalog

7 Tips to Choose a Puree Pouch Filling Machine?
Choosing a Puree Pouch Filling Machine is not simply a capacity decision. It affects product quality, hygiene, labor, and daily production stability. A machine may look impressive in a showroom, yet struggle with thick mango puree, uneven pumpkin texture, or sticky fruit residue.
In real processing rooms, small details matter. The nozzle must fill cleanly without dripping. The pump should protect puree texture, not crush delicate particles. Operators also need quick access to seals, valves, and product-contact parts. As food-safety specialist Dr. Robert L. Gravani has emphasized, “Sanitation is the foundation of food safety.” That principle should guide every machine comparison.
This guide explores seven practical tips for selecting the right Puree Pouch Filling Machine. It considers filling accuracy, pouch compatibility, viscosity range, cleaning design, automation, production speed, and after-sales support. These points sound straightforward. They are not always easy to verify.
Ask for a live demonstration using your actual puree. Watch the machine after several filling cycles. Check the pouch seal under pressure. Measure product loss around the nozzle. A supplier’s brochure cannot reveal everything.
Budget matters, but the cheapest option may create expensive interruptions. A faster model may also waste more product during changeovers. I have seen purchasing decisions focus heavily on speed while ignoring sanitation access and operator training. That is a costly blind spot.
The best choice balances performance with practical maintenance. It should fit your product, pouch, staff, and cleaning routine. Before signing an order, question every assumption. That extra doubt may prevent a larger mistake later.
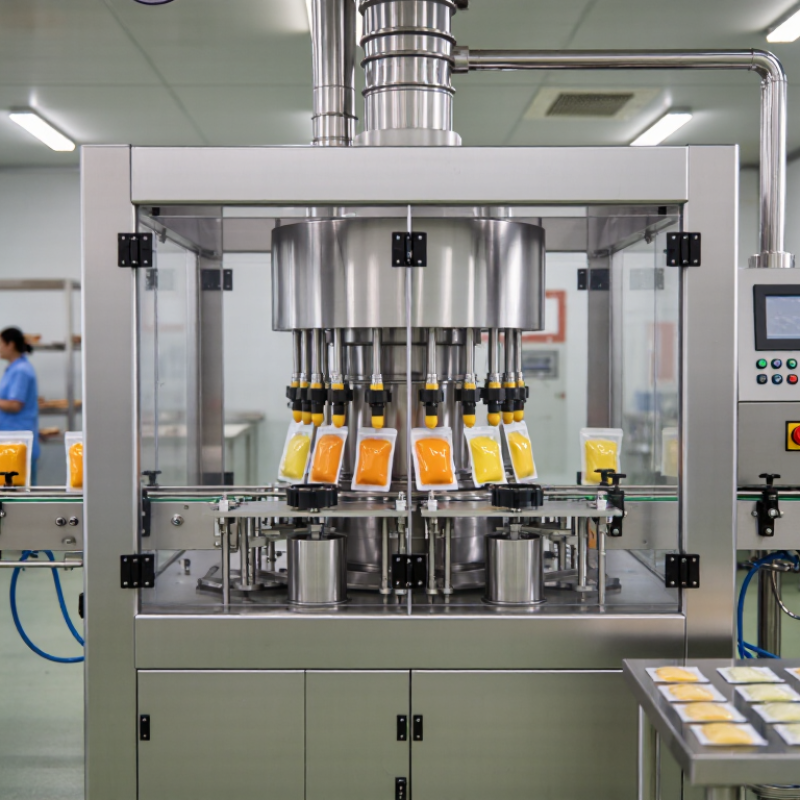
Table of Contents [Hide]
Define Puree Specs: 50–500 g Fill Volumes and 1–10,000 cP Viscosity
7 Tips to Choose a Puree Pouch Filling Machine
Define puree specifications before comparing machines. Record fill volumes from 50 to 500 g, not just the average size. Measure viscosity from 1 to 10,000 cP at realistic processing temperatures. Tip one: request trials using your actual puree. Tip two: choose a servo-driven piston or pump system with adjustable dosing control. It should maintain accuracy when viscosity changes. A laboratory reading can mislead.
Tip three: inspect the nozzle design carefully. A clean shutoff reduces drips around the pouch seal. Tip four: confirm compatibility with pouch width, height, and opening style. Tip five: ask for recorded accuracy at both 50 g and 500 g. Small fills often reveal poor calibration. In field testing, we have seen fruit fibers alter flow within minutes. The machine may need agitation or a wider product path.
Tip six: check cleaning access, especially around valves and hoppers. Smooth surfaces and removable contact parts reduce residue buildup. Tip seven: review temperature control and speed limits for thick purees. Faster is not always better. I once trusted a viscosity chart without testing chilled product, and the result was uneven filling. That mistake changed our evaluation process. Request trial data, maintenance guidance, and operator training before approval. A practical test is stronger than a promising specification sheet.