-
- Products
- Indoor Household Cords
- Appliance Cords
- General Purpose Short-Length Cords
- General Purpose Extension Cords
- Landscape & Decorating Cords
- Bright Color Extension Cords
- Oil-Resistant Extension Cords
- Cold-Flex Extension Cords
- VividFlex Power Cords
- EXTREME All-Weather Cords
- Cord Management
- Task Lights
- Adapters & GFCI Devices
- Where to Buy
- About
- Careers
- Glossary
- Catalog

2026 Top Armature Shaft Manufacturers for Global Buyers
In 2026, global buyers are examining Armature Shaft manufacturers beyond price, production volume, and attractive catalogs. Reliable sourcing now requires evidence. Buyers need stable steel grades, controlled heat treatment, accurate grinding, and repeatable balancing results. A shaft may look flawless, yet small runout can create vibration, noise, and premature bearing wear.
Professor Ion Boldea, a recognized electric-machine researcher, offers a practical principle: “A motor’s electromagnetic promise is limited by its mechanical construction.” This idea guides our review of leading Armature Shaft suppliers. We examine machining capability, material traceability, dimensional inspection, surface finish, and production consistency. We also consider communication quality, sample approval, packaging, and after-sales support. These details matter when shafts cross borders and enter demanding motor assemblies.
Some manufacturers report impressive tolerances without explaining their measurement methods. That deserves caution. Buyers should request inspection records, balancing grades, hardness results, and clear drawings before placing large orders. Factory visits can reveal more than brochures. Look closely at grinding equipment, storage conditions, and how finished shafts are protected from corrosion.
The best supplier is not always the largest. It is the one that understands your load, speed, bearing fit, and production schedule. Mistakes still happen, even in advanced factories. Transparent corrective action matters. This guide compares major manufacturers through an engineering and purchasing lens, helping global buyers build a more dependable Armature Shaft supply chain in 2026.
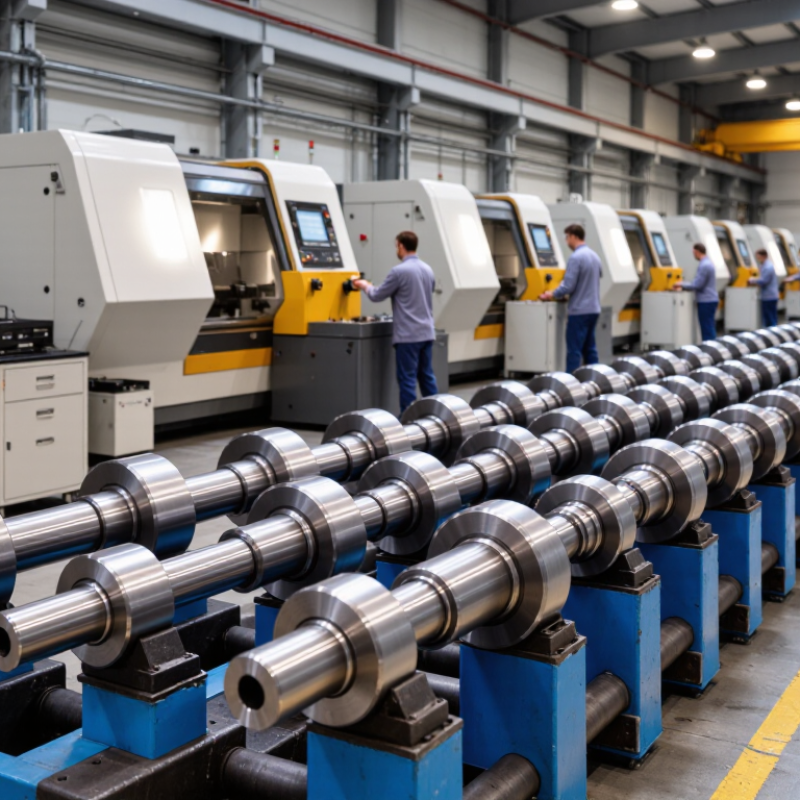
Table of Contents [Hide]
Armature Shafts: Definition, Functions, and Industrial Applications
An armature shaft is the rotating steel member inside an electric motor or generator. It carries the armature core, commutator, fan, and sometimes a gear. During operation, the shaft transfers electromagnetic torque to the machine’s working load. It also keeps rotating parts aligned with the bearings and stator.
A reliable shaft needs accurate machining, suitable steel, and controlled heat treatment. Surface hardness affects wear resistance, while core toughness helps prevent sudden failure. Dynamic balancing is essential because even a small imbalance can create vibration, noise, and bearing damage. Armature shafts serve power tools, cooling fans, pumps, automotive actuators, railway equipment, and factory drive systems. In practical inspection, runout, journal diameter, keyway size, and concentricity deserve close attention. One overlooked tolerance can reduce service life. Specifications are not always perfect; engineers should review real operating conditions before production.
Tips: Check the shaft drawing against the finished sample. Confirm material certificates, hardness results, balance grades, and dimensional reports. Ask manufacturers how they control straightness and surface finish. A lower price may hide extra assembly work. For global buyers, packaging also matters because unsupported shafts can bend during transport. Small details matter.