-
- Products
- Indoor Household Cords
- Appliance Cords
- General Purpose Short-Length Cords
- General Purpose Extension Cords
- Landscape & Decorating Cords
- Bright Color Extension Cords
- Oil-Resistant Extension Cords
- Cold-Flex Extension Cords
- VividFlex Power Cords
- EXTREME All-Weather Cords
- Cord Management
- Task Lights
- Adapters & GFCI Devices
- Where to Buy
- About
- Careers
- Glossary
- Catalog

China Best Belt Annealing Furnace Manufacturers?
China’s steel and metal-processing base creates a strong market for Belt Annealing Furnace systems. The World Steel Association reported approximately 1.019 billion tonnes of crude steel production in China during 2023. This represented more than half of global output. Such scale supports a wide supplier network, but it also makes supplier comparison difficult.
Energy performance deserves close attention. The International Energy Agency identifies iron and steel as a major industrial energy consumer, contributing roughly 8% of global final energy demand. A furnace’s heating efficiency, atmosphere control, cooling design, and heat recovery system can therefore influence operating costs. Practical buyers should request temperature-uniformity records, energy-consumption data, production references, and factory acceptance test results. A polished brochure is not enough.
This guide examines China’s best Belt Annealing Furnace manufacturers through engineering capability, product reliability, customization, certifications, and service response. Key details include strip width, line speed, furnace temperature range, protective gas control, conveyor materials, and tension stability. Manufacturers should also explain maintenance access and spare-parts availability. The shortlist is imperfect. Performance can change between projects, even within one company. Buyers should verify claims through plant audits, sample trials, and independent technical reviews. ISO 13579 guidance on industrial furnace energy efficiency offers a useful reference for comparing fuel and electricity performance. The strongest supplier is not always the largest. It is the one that delivers stable results under your actual material, speed, atmosphere, and production conditions.
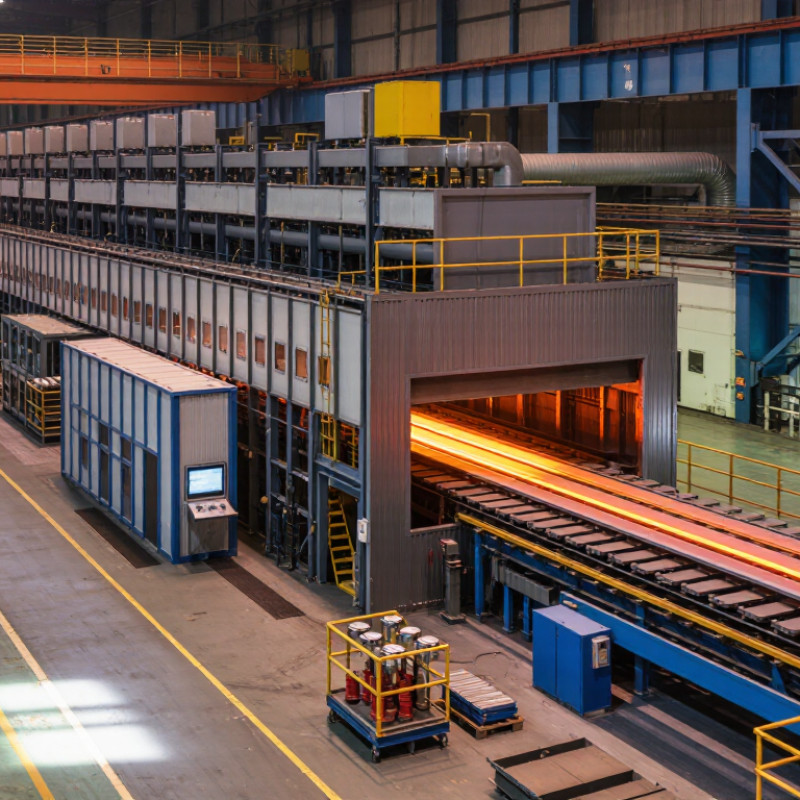
Table of Contents [Hide]
What Is a Belt Annealing Furnace and How Does It Work?
A belt annealing furnace is a continuous heat-treatment line for strip, wire, or small components. Metal travels on a heat-resistant mesh belt through controlled zones. Each zone adjusts temperature, atmosphere, and residence time. The purpose is not simply heating. It restores ductility, relieves stress, and stabilizes microstructure after forming or plating. The World Steel Association reported about 1.89 billion tonnes of global crude steel production in 2023. That scale supports demand for reliable, high-throughput annealing systems in China’s metal-processing clusters.
A typical cycle includes loading, preheating, soaking, controlled cooling, and discharge. Burners or electric elements supply heat. Fans circulate protective gas, while oxygen and dew-point sensors help limit oxidation. Belt speed determines residence time. Temperature uniformity decides whether edges and centers receive similar treatment.
Nitrogen-hydrogen mixtures may suit some alloys, but gas selection depends on surface requirements and safety design. The International Energy Agency’s Iron and Steel Technology Roadmap estimates that steelmaking produces roughly 7–9% of global energy-related carbon dioxide emissions. Small leaks matter.
When comparing Chinese manufacturers, request furnace-mapping records, atmosphere-control data, belt-life evidence, and measured energy consumption. Catalog temperature alone proves little. Test samples should match the intended belt loading and production speed. A technically attractive furnace can still underperform when the belt sags, loading changes, or cooling becomes uneven. I have seen precise specifications produce vague factory results. That gap deserves attention. Strong evaluation combines witnessed trials, calibration certificates, maintenance access, and clear acceptance criteria.