-
- Products
- Indoor Household Cords
- Appliance Cords
- General Purpose Short-Length Cords
- General Purpose Extension Cords
- Landscape & Decorating Cords
- Bright Color Extension Cords
- Oil-Resistant Extension Cords
- Cold-Flex Extension Cords
- VividFlex Power Cords
- EXTREME All-Weather Cords
- Cord Management
- Task Lights
- Adapters & GFCI Devices
- Where to Buy
- About
- Careers
- Glossary
- Catalog

China Top Barite Drywall Radiation Shielding Manufacturers
China’s Barite Drywall Radiation Shielding sector is gaining attention from hospitals, dental clinics, laboratories, and imaging facilities. These projects require more than dense wall panels. They demand measured radiation data, careful layout planning, verified material quality, and trained installation teams.
Dr. Michael G. Stabin, a respected medical physicist and radiation-protection specialist, has stated, “Shielding design must be based on exposure assessment, not material claims alone.” This principle matters when comparing Chinese manufacturers. Barite drywall may combine gypsum board with high-density barite compounds. Its performance depends on density, thickness, joints, fasteners, openings, and workmanship. A small gap around a service pipe can weaken an otherwise strong barrier.
Details matter here.
Leading suppliers should provide clear technical data, batch consistency records, fire-performance information, and installation guidance. They should also explain whether their products suit diagnostic X-ray rooms, CT areas, laboratories, or other controlled environments. One product cannot fit every project. That is easy to forget.
A reliable manufacturer should cooperate with qualified shielding designers and follow the project’s approved radiation assessment. Factory photographs are useful, but they are not proof. Independent testing, traceable documentation, and practical installation experience offer stronger evidence. Even experienced buyers can overlook acoustic performance, wall loading, moisture resistance, or future equipment changes.
This guide examines China’s top Barite Drywall Radiation Shielding manufacturers through an E-E-A-T-focused lens. It considers technical credibility, manufacturing experience, documentation quality, and customer support. Some claims still require verification. That uncertainty should remain visible, not hidden behind polished marketing language.
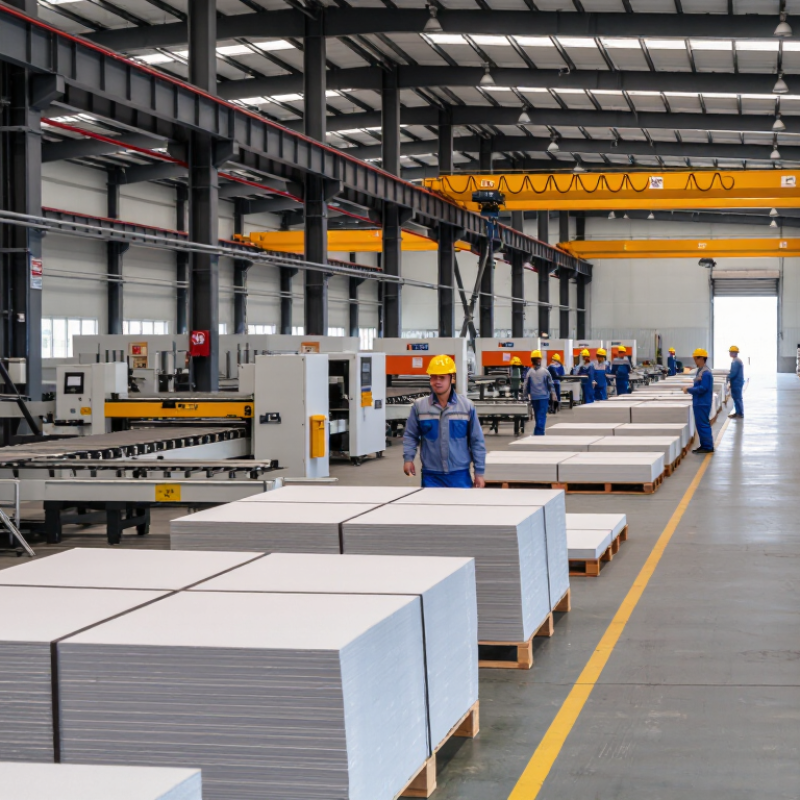
Table of Contents [Hide]
Barite Drywall Radiation Shielding: Purpose and Key Properties
Barite Drywall Radiation Shielding: Purpose and Key Properties
Barite drywall uses high-density barium sulfate to reduce scattered and direct diagnostic X-ray radiation. Its purpose is controlled attenuation, not complete elimination. NCRP Report No. 147 states that shielding design depends on workload, tube voltage, distance, occupancy, and use factors. Workload is commonly expressed in mA-minutes per week. Therefore, one thickness cannot serve every room. IAEA Safety Reports Series No. 47 also supports calculation-based designs and post-installation verification.
Barite-filled panels are denser than standard gypsum boards, often reaching about 2.8–3.5 g/cm³, depending on formulation. This density improves attenuation but increases wall loads. Joints, service penetrations, corners, and door frames remain vulnerable points. NCRP guidance emphasizes continuous shielding surfaces and qualified assessment. In practice, drawings may look complete, yet one poorly sealed outlet can weaken local protection. Performance data should come from tested assemblies, not density alone. That distinction is easy to miss.
Tips: Request a radiation physicist’s shielding calculation before purchasing panels. Check tested lead-equivalence data at the planned kVp. Confirm substrate capacity and lifting access. Photograph every joint before closing the wall. A small omission can become expensive. Recheck shielding after equipment installation.