-
- Products
- Indoor Household Cords
- Appliance Cords
- General Purpose Short-Length Cords
- General Purpose Extension Cords
- Landscape & Decorating Cords
- Bright Color Extension Cords
- Oil-Resistant Extension Cords
- Cold-Flex Extension Cords
- VividFlex Power Cords
- EXTREME All-Weather Cords
- Cord Management
- Task Lights
- Adapters & GFCI Devices
- Where to Buy
- About
- Careers
- Glossary
- Catalog

Top FR209E Type Coupler Body Manufacturers Worldwide
The global rail equipment market is expanding, but coupler components remain a demanding specialist segment. UNIFE’s World Rail Market Study 2024 reports continued investment in rolling stock, rail infrastructure, and aftermarket services across major regions. That growth increases demand for reliable replacement parts, including the Fr209e Type Coupler Body.
This component must withstand repeated coupling forces, vibration, impact, and harsh outdoor conditions. Manufacturers therefore need controlled casting or forging processes, accurate machining, traceable materials, and documented inspection results. Details matter. Records matter. Buyers should examine dimensional reports, hardness results, non-destructive testing, coating performance, and production consistency before selecting a supplier.
Industry expectations also connect with international quality practices. ISO 9001 supports controlled production systems, while EN 15085 may be relevant when welding activities affect railway components. AAR requirements can matter for North American applications, although compliance depends on the vehicle platform and purchasing specification. The European Railway Agency’s safety framework also reinforces the importance of traceability and risk-based engineering.
A supplier may look impressive on paper and still deliver uneven batches. That is the uncomfortable part. Manufacturer comparisons should therefore include factory capability, engineering experience, inspection equipment, export history, and after-sales responsiveness. Public company profiles are useful, but independent audits and sample verification provide stronger evidence.
This guide examines leading Fr209e Type Coupler Body manufacturers worldwide through practical purchasing criteria. It considers material control, manufacturing capacity, certification evidence, customization support, delivery reliability, and lifecycle value. Market rankings are never permanent. Performance data, customer feedback, and technical transparency should influence every final decision.
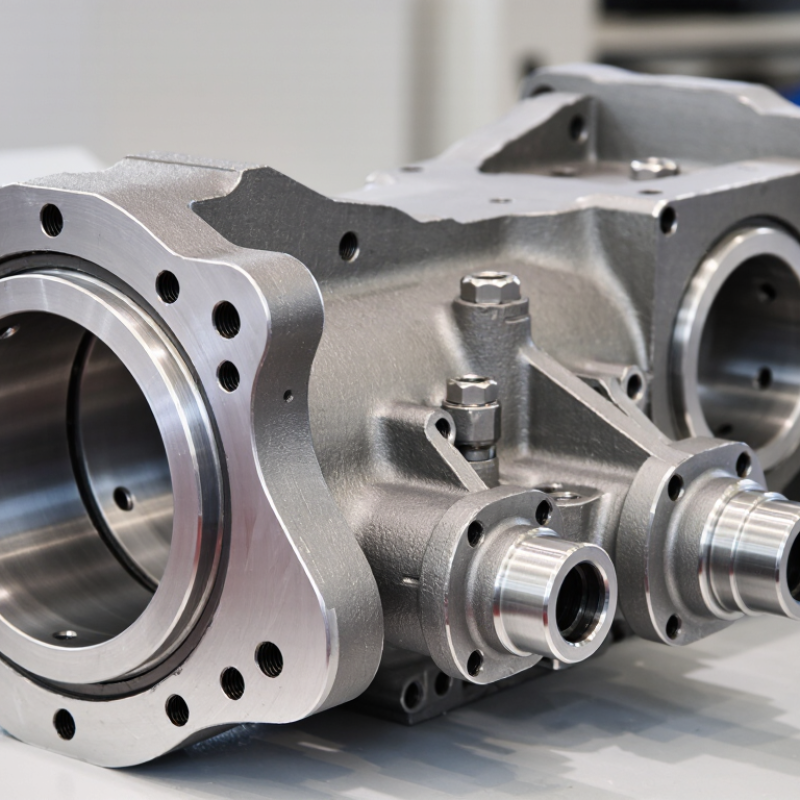
Table of Contents [Hide]
FR209E Coupler Bodies: Definition, Function, and Industry Terminology
FR209E Coupler Bodies: Definition, Function, and Industry Terminology
An FR209E coupler body is the main structural housing in a compatible rail freight coupler assembly. It transfers pulling and pushing forces between connected vehicles. The body also supports the knuckle, pivot area, lock components, and draft gear connection. In practical inspections, technicians examine the shank, casting surfaces, pin bores, and draft pocket. Small surface defects can become serious under repeated impact loads.
Industry terminology is not perfectly uniform. Some suppliers describe the part as a coupler body, while others use housing, head-and-shank casting, or coupler casting. These terms may not identify identical components. Buyers should compare the FR209E designation with approved drawings, interface dimensions, material requirements, and heat-treatment records. That detail is easy to miss.
Qualified manufacturers typically control casting quality, machining accuracy, and inspection traceability. Dimensional checks confirm coupler height, mounting interfaces, and alignment with adjoining parts. Non-destructive testing may help detect cracks or internal discontinuities. Material certificates provide evidence of the specified steel grade and processing route. In my experience, a clean surface does not prove structural reliability. Verification must follow documented procedures. The designation alone is not enough. Each production batch should remain traceable from raw material to final inspection. Some terminology still varies between regions, so technical teams should confirm every critical definition before ordering.
Top FR209E Type Coupler Body Manufacturers Worldwide - FR209E Coupler Bodies: Definition, Function, and Industry Terminology
| Data Dimension | FR209E Coupler Body Reference | Industry Meaning | Practical Verification Point |
|---|---|---|---|
| Product category | Railway rolling-stock coupler body | The main structural casting or forging that carries the coupler head, shank, locking mechanism, and draft loads. | Confirm the application, coupler system, drawing revision, and interface geometry before ordering. |
| Designation | FR209E type | A product or drawing designation used to identify a particular coupler-body configuration; the designation alone does not establish every dimensional or material requirement. | Request the controlling technical drawing, revision level, and applicable railway specification. |
| Primary function | Transmit tensile and compressive train forces | The body transfers coupler forces into the yoke, draft gear, center sill, or other supporting structure. | Check static strength, fatigue requirements, and compatibility with the draft system. |
| Coupling interface | Automatic mechanical coupling face | The front portion engages with the mating coupler and normally includes the knuckle pocket, lock region, guard arm, and related contours. | Verify coupler contour, knuckle geometry, locking clearances, and mating-coupler compatibility. |
| Rear interface | Shank, yoke, and draft-gear connection | The rear section connects the coupler body to the yoke and energy-absorbing draft arrangement. | Measure shank section, pin-hole location, wear surfaces, and available longitudinal travel. |
| Typical material family | Cast or forged carbon and low-alloy steel | Railway coupler bodies commonly use high-strength ferrous alloys selected for impact toughness, wear resistance, and fatigue performance. | Confirm the specified grade, chemical composition, heat treatment, hardness, and impact properties. |
| Manufacturing route | Precision casting or closed-die forging, followed by machining | The process must produce sound load-bearing sections, accurate coupling contours, and controlled dimensional tolerances. | Review process qualification, melt or heat traceability, machining control, and non-destructive testing records. |
| Critical load areas | Shank transition, pin-hole region, knuckle pocket, guard arm, and draft-stop surfaces | These areas experience concentrated tensile, compressive, bending, impact, and fatigue stresses during service. | Inspect for cracks, sharp transitions, porosity, dimensional wear, and surface damage. |
| Common components used with the body | Knuckle, lock, lift mechanism, lock-lifter, knuckle pin, yoke, draft gear, and carrier | The coupler body is only one part of the complete coupler assembly and cannot be evaluated independently from its interfaces. | Check interchangeability, pin diameters, clearances, wear limits, and assembly orientation. |
| Relevant performance requirements | Strength, toughness, fatigue resistance, wear resistance, and dimensional stability | Performance is determined by design loads, operating environment, material condition, and maintenance practice. | Use documented test procedures and acceptance criteria rather than relying only on nominal dimensions. |
| Quality-control methods | Visual inspection, dimensional inspection, hardness testing, ultrasonic testing, magnetic-particle testing, and mechanical testing | Non-destructive and destructive tests help identify surface cracks, internal discontinuities, incorrect heat treatment, and material nonconformity. | Define sampling frequency, acceptance limits, calibration requirements, and certificate format in the purchase specification. |
| Surface condition | Machined interfaces with controlled casting or forging surfaces | Coupling contours, pin bores, wear surfaces, and draft interfaces require tighter control than non-functional external surfaces. | Specify roughness, burr removal, dimensional tolerance, and permissible surface imperfections. |
| Industry terminology | Coupler body, automatic coupler, shank, head, knuckle pocket, lock, yoke, draft gear, carrier, draft stop, and coupler contour | These terms describe the structural part, mating parts, load path, and operating mechanism of the coupler assembly. | Use the terminology defined by the applicable railway standard or approved technical drawing. |
| Supplier evaluation criteria | Technical conformity, production capacity, traceability, inspection capability, delivery reliability, and after-sales support | A qualified supplier should demonstrate repeatable production and documented compliance for safety-critical railway components. | Request quality-system certificates, sample inspection reports, material certificates, test records, and reference approvals. |
| Purchasing documentation | Approved drawing, specification, inspection plan, packing requirements, and traceability requirements | Complete documentation reduces the risk of receiving a dimensionally similar but technically incompatible coupler body. | Include part designation, revision, quantity, service application, testing requirements, and acceptance procedure. |
| Important technical limitation | FR209E dimensions and material details are drawing-specific | A type designation should not be treated as a universal dimensional standard unless supported by an authorized specification. | Obtain the latest controlled drawing and written confirmation of interchangeability before production or replacement. |
Technical note: FR209E is presented here as a type designation for a railway coupler body. Exact dimensions, material grade, load ratings, inspection criteria, and interchangeability must be confirmed against the current authorized engineering drawing and applicable railway requirements.