-
- Products
- Indoor Household Cords
- Appliance Cords
- General Purpose Short-Length Cords
- General Purpose Extension Cords
- Landscape & Decorating Cords
- Bright Color Extension Cords
- Oil-Resistant Extension Cords
- Cold-Flex Extension Cords
- VividFlex Power Cords
- EXTREME All-Weather Cords
- Cord Management
- Task Lights
- Adapters & GFCI Devices
- Where to Buy
- About
- Careers
- Glossary
- Catalog

Top Carbon Steel Pipe Manufacturers in the World
Carbon Steel Pipe remains essential to industries that move fluids, gases, and materials under demanding conditions. Its strength, weldability, and range of available grades make it a practical choice for construction, energy, water systems, and manufacturing. Yet no single pipe suits every project. Wall thickness, diameter, grade, operating pressure, and environmental exposure all shape the right specification.
This guide explores leading Carbon Steel Pipe manufacturers around the world and the factors that distinguish their offerings. A manufacturer’s reputation matters, but so do production capacity, quality controls, technical support, and delivery reliability. Buyers should also examine applicable product standards, inspection records, and traceability documents rather than relying on broad marketing claims. Details count.
The companies covered serve different markets and project needs. Some focus on large-diameter line pipe, while others offer products for structural or industrial applications. Their strengths can vary by region and product category, so a global ranking should not be treated as a universal verdict. That distinction is easy to overlook.
Comparisons in this article provide a starting point, not a substitute for engineering review or supplier qualification. Confirm current specifications directly with manufacturers, since product ranges and certifications may change. Even a well-known supplier may not be the best fit for a particular project. That is worth remembering. By weighing documented capabilities against actual operating requirements, readers can make a more informed shortlist and ask better questions before purchasing.
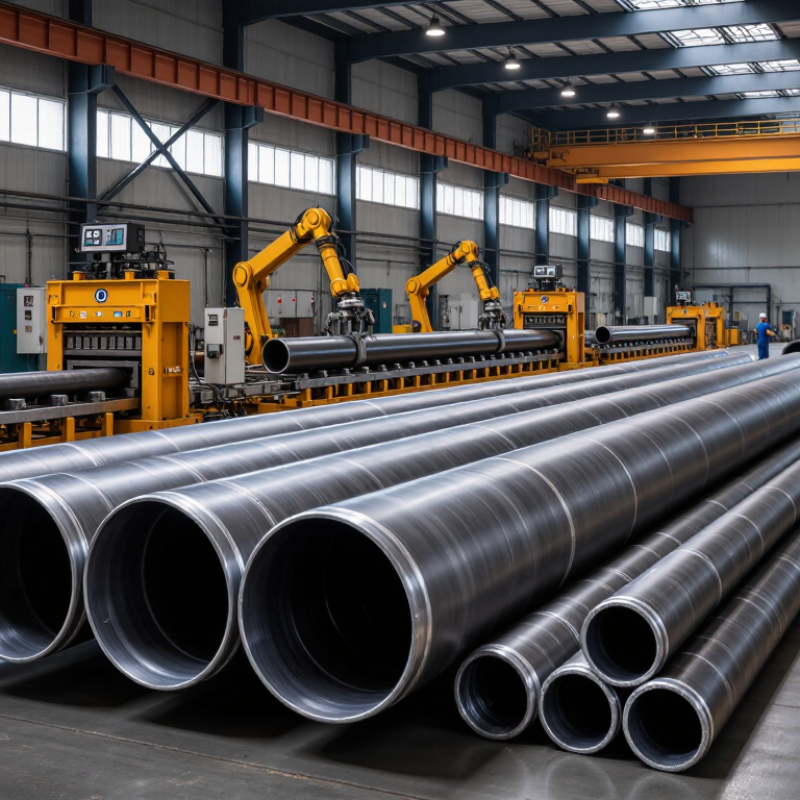
Table of Contents [Hide]
Carbon Steel Pipe Manufacturing: Products, Processes, and Applications
Carbon steel pipe manufacturing begins with selecting steel grades that match pressure, temperature, and service conditions. Pipes are commonly made by forming and welding steel plate or strip, or by piercing and rolling solid billets into seamless lengths. Each route has different costs and performance characteristics. Neither is universally better.
During production, mills control dimensions, weld quality, and material properties. Welded pipes may undergo ultrasonic or radiographic inspection, while seamless pipes are checked for surface and dimensional defects. Heat treatment can help achieve specified strength or toughness. Testing matters. Buyers should review applicable standards, wall thickness, outside diameter, and inspection records rather than relying on appearance alone. A clean surface can still hide a defect.
Applications range from water transmission and building supports to industrial process lines and energy infrastructure. The operating environment shapes the choice: corrosive fluids may require coatings or other protective measures, while high-pressure service demands careful grade and thickness selection. Installation also affects reliability. Poor alignment, unsuitable joining methods, or damage to a coating can undermine a well-made pipe. Even detailed specifications cannot remove every uncertainty; field conditions and maintenance practices still deserve attention.
Top Carbon Steel Pipe Manufacturers in the World - Carbon Steel Pipe Manufacturing: Products, Processes, and Applications
This overview compares common carbon steel pipe product categories and manufacturing routes. It is not a company ranking; actual availability, dimensions, grades, and qualification requirements vary by producer and order.
| Product Category | Typical Manufacturing Process | Common Standards and Specifications | Typical Characteristics | Common Applications |
|---|---|---|---|---|
| Seamless carbon steel pipe | A solid steel billet is heated, pierced, and rolled or drawn into a hollow tube. Finishing may include heat treatment, sizing, and inspection. | ASTM A106/A106M; ASTM A53/A53M Type S; API Specification 5L | Has no longitudinal weld seam. Available in multiple grades and schedules; suitability depends on the specified grade, dimensions, and service conditions. | Oil and gas systems, refineries, power plants, and other pressure or process piping services. |
| ERW pipe | Flat steel strip is formed into a cylinder, and its edges are joined by electric resistance welding. The weld is typically inspected and finished in line. | ASTM A53/A53M Type E; API Specification 5L | Longitudinally welded pipe produced from coil or strip. Production efficiency and available dimensions depend on the mill and specification. | Water and gas distribution, structural uses, and specified line-pipe services. |
| Longitudinal SAW pipe | Steel plate is formed into a pipe shape, then the longitudinal joint is welded using a submerged arc welding process. | API Specification 5L; ASTM A671 or ASTM A672, as applicable to the ordered service | Large-diameter pipe can be made from plate. The applicable specification defines requirements such as grade, testing, and service conditions. | Transmission pipelines, water infrastructure, and pressure-service projects where the selected specification is suitable. |
| Spiral SAW pipe | Steel strip is helically formed into a cylinder and joined along a spiral seam by submerged arc welding. | API Specification 5L and project-specific requirements, where applicable | Manufactured from coiled strip; diameter and wall thickness ranges depend on the production line and order specification. | Water transmission, infrastructure, and selected pipeline projects. |
| Low-temperature carbon steel pipe | Produced as seamless or welded pipe, with grade-specific material controls and testing. Heat treatment and impact testing depend on the specification and grade. | ASTM A333/A333M | Specified for low-temperature service; required impact-test temperatures and acceptance criteria are grade- and order-dependent. | Refrigeration and process piping, and other services requiring material performance at low temperatures. |
| Pressure-service welded pipe | Made by a specified welding route, such as electric-fusion welding, with inspection and testing requirements set by the applicable specification. | ASTM A671/A671M; ASTM A672/A672M | These specifications cover electric-fusion-welded steel pipe for defined pressure-service conditions; material class and testing requirements vary by designation. | Pressure piping in power, industrial, and process facilities when the specified class and service conditions are appropriate. |
| General-purpose carbon steel pipe | Can be manufactured as seamless or welded pipe, depending on the type and requirements ordered. | ASTM A53/A53M | Specification covers black and hot-dipped, zinc-coated welded and seamless steel pipe in the specified grades and types. | Mechanical and pressure applications, as well as ordinary uses in steam, water, gas, and air lines, subject to specification limits. |
| Line pipe | Seamless or welded production routes may be used. Manufacturing controls, inspection, and testing are specified by the ordered product level and grade. | API Specification 5L | Designed for pipeline transportation applications. Grade, dimensions, manufacturing route, and supplementary requirements are selected for the project. | Oil, gas, and other pipeline transportation systems, subject to the applicable design code and service requirements. |