-
- Products
- Indoor Household Cords
- Appliance Cords
- General Purpose Short-Length Cords
- General Purpose Extension Cords
- Landscape & Decorating Cords
- Bright Color Extension Cords
- Oil-Resistant Extension Cords
- Cold-Flex Extension Cords
- VividFlex Power Cords
- EXTREME All-Weather Cords
- Cord Management
- Task Lights
- Adapters & GFCI Devices
- Where to Buy
- About
- Careers
- Glossary
- Catalog

Top 10 Hardening Oven Manufacturers for Global Buyers
Choosing the right Hardening Oven is rarely a simple purchasing exercise. Global buyers must examine temperature uniformity, furnace capacity, atmosphere control, loading methods, energy use, and after-sales support. A machine may look impressive in a brochure, yet perform poorly when production loads vary. That difference matters on a busy factory floor.
Dr. George E. Totten, a widely recognized heat-treatment authority, has described heat treatment as “both a science and an art.” This view remains practical. Operators need reliable data, but they also need experience with steel grades, part geometry, quenching behavior, and process changes. A small temperature deviation can affect hardness, distortion, or surface quality. The best manufacturers provide calibrated controls, clear maintenance guidance, documented testing, and responsive technical assistance.
This Top 10 Hardening Oven Manufacturers for Global Buyers guide compares suppliers through a practical lens. It considers engineering capability, product consistency, customization, safety features, international service, and long-term operating value. It also looks beyond polished specifications. Some manufacturers offer excellent equipment but limited regional support. Others provide strong service while lacking flexibility for unusual workloads. Buyers should reflect on these trade-offs before choosing.
No ranking can fit every factory. Production volume, material type, certification needs, and available floor space change the decision. A careful buyer should request performance records, inspect references, and clarify warranty conditions. That extra effort may feel slow. It can prevent expensive surprises later.
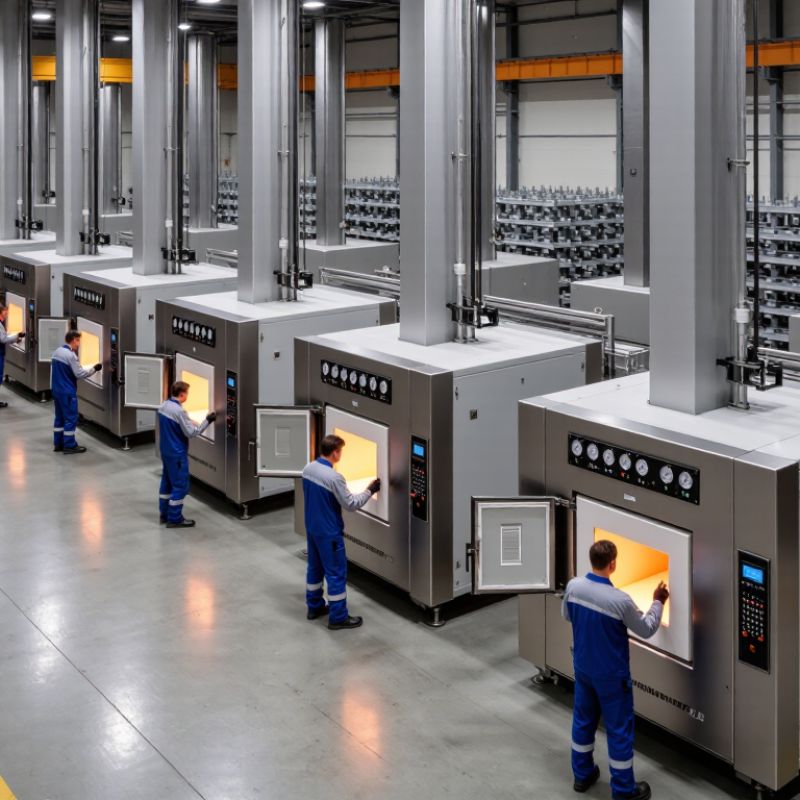
Table of Contents [Hide]
Hardening Ovens: Purpose, Design, and Industrial Applications
Hardening Ovens: Purpose, Design, and Industrial Applications
Hardening ovens heat steel and other alloys to controlled temperatures before quenching or tempering. This cycle changes hardness, strength, wear resistance, and dimensional stability. In practice, operators watch more than the setpoint. Load spacing, air movement, door openings, and thermocouple placement can alter results. Uniformity matters. A small hot zone can create rejected parts.
Modern designs commonly use forced convection, programmable controls, insulated chambers, and atmosphere management. Some systems connect heating, quenching, and data logging within one production line. The U.S. Department of Energy states that process heating represents about 51% of industrial energy use in the United States. Therefore, insulation, recovery cycles, and accurate temperature control affect both cost and emissions. The International Energy Agency also identifies industry as responsible for roughly 37% of global final energy consumption, reinforcing the value of efficient thermal equipment.
Applications include automotive components, cutting tools, springs, fasteners, aerospace parts, and general machinery. Buyers should examine temperature uniformity, usable chamber volume, ramp rates, cooling capability, maintenance access, and validation records. ISO 13577 provides safety guidance for industrial furnaces and associated thermal processing equipment. Yet compliance alone does not guarantee good production. A technically impressive oven may still perform poorly with uneven loading or weak operator training. That is the uncomfortable part. Equipment selection requires production trials, not only catalog comparisons. Reliable suppliers should provide test data, calibration procedures, service support, and clear limits for each material and recipe.