-
- Products
- Indoor Household Cords
- Appliance Cords
- General Purpose Short-Length Cords
- General Purpose Extension Cords
- Landscape & Decorating Cords
- Bright Color Extension Cords
- Oil-Resistant Extension Cords
- Cold-Flex Extension Cords
- VividFlex Power Cords
- EXTREME All-Weather Cords
- Cord Management
- Task Lights
- Adapters & GFCI Devices
- Where to Buy
- About
- Careers
- Glossary
- Catalog

Top Interlock Folding Machine Manufacturers Worldwide
An Interlock Folding Machine helps manufacturers produce consistent folds in garments and other textile products. In a busy workshop, fabric moves through guides, rollers, and folding stations before reaching the next production step. A steady feed can reduce uneven edges and repetitive handwork. Small details matter. Even a minor adjustment to tension or alignment may affect the finished fold.
This guide introduces leading Interlock Folding Machine manufacturers worldwide and the practical factors buyers can compare. These include machine configuration, supported fabric types, production speed, changeover requirements, operator access, and the availability of spare parts. A clear specification sheet is useful, but it cannot answer every question. Ask how the machine handles your actual material, and request a demonstration using comparable fabric whenever possible. Check service arrangements, too.
Manufacturer choice depends on the production environment, not just the brochure. A compact operation may value simple setup and accessible controls, while a larger line may prioritize integration and repeatable output. No supplier is perfect. A shortlist can still miss important differences in training, maintenance, or delivery support. Verify claims with documentation and, where practical, customer references. Then compare the machine against your own workflow. The right choice should fit the work, the operators, and the resources available—not merely an impressive specification.
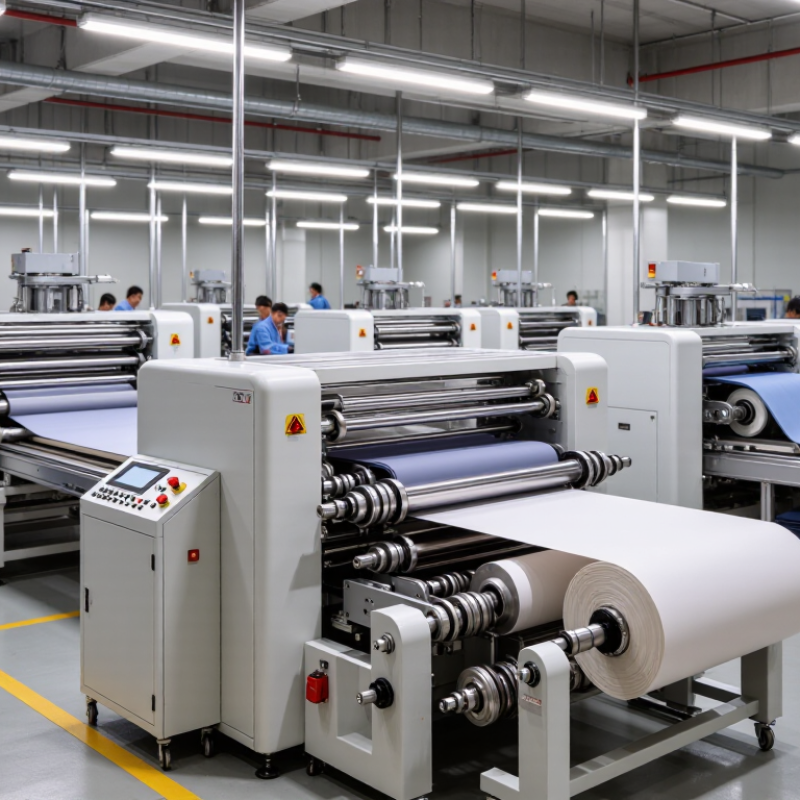
Table of Contents [Hide]
Understanding Interlock Folding Machines and Their Role
Top Interlock Folding Machine Manufacturers Worldwide
Understanding Interlock Folding Machines and Their Role
Interlock folding machines convert pre-creased carton blanks into stable packages without relying entirely on adhesive. They fold panels, guide locking tabs, and close the base through controlled mechanical movement. This design suits takeaway cartons, shipping boxes, and retail packaging that needs quick assembly.
In practical production, operators feed flat blanks onto a belt conveyor. Folding rails then raise side panels, while forming tools push the locking flaps into place. Sensors check blank position and reduce jams caused by warped board. A reliable machine should handle common paperboard grades, maintain consistent pressure, and allow tool-free adjustments where possible.
Speed matters, but it is not everything. A fast line with poor alignment creates crushed corners and expensive waste. I have seen minor crease variation disrupt an entire batch. That detail is easy to overlook. Regular cleaning also protects folding belts from paper dust and improves repeatability. Manufacturers with strong engineering records usually provide clear manuals, spare-part support, and operator training. Still, buyers should test their own carton samples before choosing equipment. Laboratory performance can differ from a busy factory floor. Temperature, humidity, board stiffness, and operator habits all influence final results.