-
- Products
- Indoor Household Cords
- Appliance Cords
- General Purpose Short-Length Cords
- General Purpose Extension Cords
- Landscape & Decorating Cords
- Bright Color Extension Cords
- Oil-Resistant Extension Cords
- Cold-Flex Extension Cords
- VividFlex Power Cords
- EXTREME All-Weather Cords
- Cord Management
- Task Lights
- Adapters & GFCI Devices
- Where to Buy
- About
- Careers
- Glossary
- Catalog

China Top 10 Thread Milling Insert Manufacturers?
China has become a major source of precision cutting tools, including Thread Milling Insert products for automotive, aerospace, mold, and general machining applications. However, supplier quality varies widely. A polished catalog does not always reflect stable production or consistent tool life.
This guide examines ten leading Chinese manufacturers through practical purchasing criteria. The review considers insert geometry, carbide grades, coating options, thread profiles, dimensional accuracy, and production capacity. It also looks at inspection systems, sample support, export experience, and technical communication. These details matter when a small insert must cut clean threads inside hardened steel or aluminum components.
Some manufacturers focus on standard metric sizes. Others provide custom profiles, special pitches, or application-specific coatings. Tool users should compare actual test results rather than rely only on impressive claims. Cutting speed, feed rate, workpiece material, and machine rigidity can change performance significantly.
Supplier verification remains essential. Certifications can support credibility, but they should be checked against current factory practices. Product samples, inspection reports, and clear tolerance data often reveal more than promotional language. The ranking may not fit every buyer, because price, lead time, and technical requirements differ.
There is no perfect supplier.
The following manufacturers are assessed with a balanced approach. Their strengths, limitations, product ranges, and service capabilities are considered together. Readers can use this information to shortlist suitable partners and request meaningful technical evidence before placing an order.
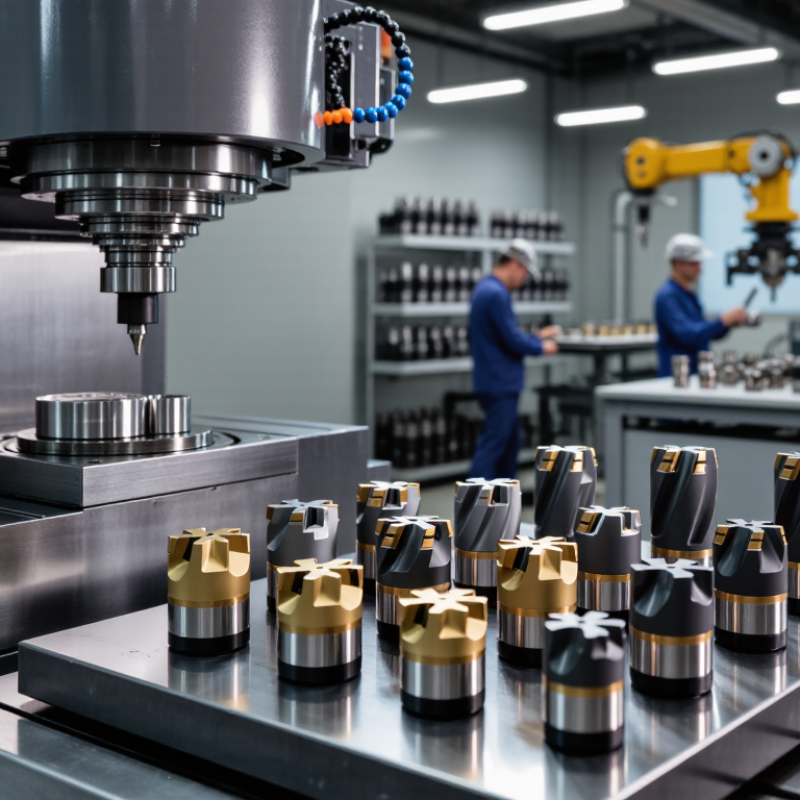
Table of Contents [Hide]
Scope and Definition: What Qualifies as a Chinese Thread Milling Insert Manufacturer?
A Chinese thread milling insert manufacturer should do more than list products online. It should control essential production stages inside China, including insert design, material preparation, grinding, coating coordination, and final inspection. A trading company may offer useful sourcing services, but it should not be classified as a manufacturer without verifiable factory involvement.
The qualification begins with technical capability. A credible manufacturer can explain thread profiles, pitch ranges, insert geometries, cutting depths, and suitable workpiece materials. It should provide dimensional reports, batch traceability, coating information, and inspection records. Samples should match drawings, not merely photographs. Small details matter. A clean edge, stable tolerance, and consistent hole finish often reveal more than a polished catalog.
Practical experience also matters. The supplier should discuss chip control, cutting speed, coolant use, and common failure patterns during trial machining. Factory audits, production videos, and independent sample testing strengthen reliability. Still, no supplier is perfect. Delivery schedules can slip, and trial results may differ between machines, operators, and materials. That weakness deserves honest discussion. A serious Chinese manufacturer accepts technical questions, investigates failed inserts, and adjusts production records instead of hiding behind sales language. Its status depends on repeatable manufacturing evidence, not a country label or a large product list.