-
- Products
- Indoor Household Cords
- Appliance Cords
- General Purpose Short-Length Cords
- General Purpose Extension Cords
- Landscape & Decorating Cords
- Bright Color Extension Cords
- Oil-Resistant Extension Cords
- Cold-Flex Extension Cords
- VividFlex Power Cords
- EXTREME All-Weather Cords
- Cord Management
- Task Lights
- Adapters & GFCI Devices
- Where to Buy
- About
- Careers
- Glossary
- Catalog

Which Is the Best China Nozzle Cutting Machine?
Choosing the best China Nozzle Cutting Machine requires more than comparing prices, power ratings, or attractive product photos. The right machine must match your material, production volume, nozzle design, and maintenance skills. A workshop cutting stainless steel sheets may need different performance from a factory processing carbon steel every day. Small details matter. Nozzle diameter, centering accuracy, cooling stability, and replacement-part availability can directly affect cut quality.
Laser-cutting specialist John Powell has stated, “The laser beam is only as good as the system that delivers it.” This principle applies closely to every Nozzle Cutting Machine. A powerful laser cannot compensate for poor nozzle alignment, unstable gas flow, or careless calibration. During practical testing, operators should inspect edge smoothness, piercing time, slag buildup, and beam consistency across repeated jobs. Results should be recorded, not guessed.
There is no flawless machine for every buyer. Some Chinese manufacturers offer excellent automation but limited technical support in overseas markets. Others provide reliable cutting performance, yet their software may feel less refined. That difference can become expensive after installation. Buyers should examine factory experience, certification records, warranty terms, training quality, and real customer feedback. A factory visit or live cutting test is even better.
This guide compares leading options through an experience-based and technical lens. It also recognizes an uncomfortable point: the cheapest machine may not be the most economical choice. Long-term reliability, service response, and nozzle consistency often matter more than the first quotation.
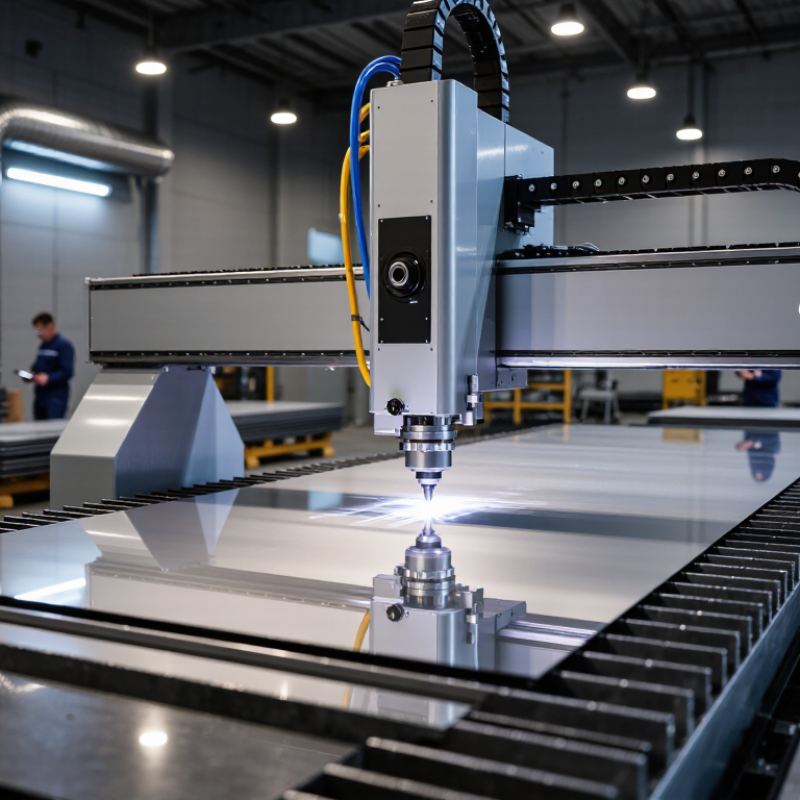
Table of Contents [Hide]
What Is a China Nozzle Cutting Machine?
A China nozzle cutting machine is a computer-controlled system designed to produce precise nozzles from metal or other suitable materials. In many workshops, it uses laser, plasma, or mechanical cutting technology. The correct process depends on material thickness, nozzle geometry, and required tolerance.
The machine usually combines a cutting head, motion table, control software, and fixture. The fixture holds each workpiece firmly during cutting. This matters because even slight movement can create an uneven opening. Operators commonly adjust cutting speed, power, gas pressure, and focal position. Small changes can affect edge quality.
A reliable evaluation should begin with sample cutting, not promises. Ask for measured results, repeatability records, and compatible material data. Check whether the control system supports the shapes your production actually needs. Maintenance access also matters. Dust, heat, and metal particles can reduce performance over time.
Not every machine is equal.
In practical testing, inspect the finished nozzle under magnification. Look for burrs, taper, cracks, or heat discoloration. A clean edge may improve airflow and service life, but cutting quality is only one factor. Tool stability, operator training, spare parts, and safety controls also influence the final result. The term “China nozzle cutting machine” describes an origin and machine category, not a guaranteed level of quality. A careful buyer should verify each technical claim. Mistakes happen, especially when specifications are copied without testing.